We have compiled a list of manufacturers, distributors, product information, reference prices, and rankings for Surveillance system.
ipros is IPROS GMS ・ IPROS One of the largest technical database sites in Japan that collects information on.

Surveillance system Product List and Ranking from 425 Manufacturers, Suppliers and Companies | IPROS GMS

Last Updated: Aggregation Period:Sep 30, 2026~Oct 27, 2026
This ranking is based on the number of page views on our site.

Surveillance system Manufacturer, Suppliers and Company Rankings

Last Updated: Aggregation Period:Sep 30, 2026~Oct 27, 2026
This ranking is based on the number of page views on our site.

  1. 因幡電機産業 産機カンパニー Osaka//Trading company/Wholesale
  2. グリッドリンク IoTプラットフォーム事業部 Tokyo//IT/Telecommunications
  3. アメロイド Kanagawa//Industrial Machinery
  4. 4 HexaCORE Co., Ltd. (formerly Chuo Seisakusho Co., Ltd.) Head Office and Factory Miyagi//Industrial Electrical Equipment
  5. 5 MI Tokyo//IT/Telecommunications

Surveillance system Product ranking

Last Updated: Aggregation Period:Sep 30, 2026~Oct 27, 2026
This ranking is based on the number of page views on our site.

  1. Automatic recording of video before and after an error occurs on site: "Choco Stop Watcher II" 因幡電機産業 産機カンパニー
  2. Remote monitoring of various factory equipment metrics in real time! *Consultations are currently being accepted. アメロイド
  3. Is your factory's digital transformation only ending with "visualization"? MI
  4. 4 Remote monitoring system 'C2-Connect' for equipment such as pumps. HEISHIN Ltd. Tokyo Branch
  5. 5 [Silent, No Emissions] Battery-Powered Transport Monorail (with Regenerative Function) 松永通信 北条支店

Surveillance system Product List

781~810 item / All 951 items

Displayed results

Remote measurement of direct current | Daily check of backup power supply for base stations

Daily checks of the base station's backup power supply. Continuously monitor the equipment circuit with a DC current sensor that supports 30A to 500A.

Are you able to continuously monitor the direct current of mobile phone base stations and communication facilities, not just during inspections? Relying solely on instantaneous measurements may overlook changes due to time of day or load conditions. The "iDC-SVS4" is a sensor that supports 30A, 50A, 100A, 250A, and 500A, allowing for continuous measurement of direct current and sending measurement data to a monitoring server. You can remotely check the current value, load fluctuations, and past history, and in combination with monitoring software, it can also provide notifications based on set thresholds. It is compatible with initial installation in our distribution boards and supports the reduction of on-site work through load testing and equipment settings before shipment. Usage Scenarios: - Monitoring direct current of mobile phone base stations and communication facilities - Checking current values and history of direct load circuits for backup power supplies - Confirming inspection targets and notification status before on-site visits Expected Benefits from Implementation: - Understanding current changes over time outside of patrols - Consolidating measurement information from multiple circuits - Organizing inspection targets and confirmation details in advance to streamline facility management We will propose configurations based on monitoring targets, number of circuits, cable diameter, and installation environment.
  • Ammeter
  • Power Monitoring Equipment
  • Remote Control
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Continuous measurement of direct current | Time-series management of the DC load for emergency power supply

Manage the DC load of the emergency power supply over time. Continuously monitor the equipment circuit with a DC current sensor that supports 30A to 500A.

To streamline the inspection of disaster prevention bases and important facilities, it is effective to identify equipment with changes from current history and prioritize them, rather than checking all circuits at the same frequency. The "iDC-SVS4" is a sensor that supports 30A, 50A, 100A, 250A, and 500A, continuously measuring direct current and sending the measurement data to a monitoring server. It allows remote confirmation of current values, load fluctuations, and past history, and, in combination with monitoring software, can respond to notifications based on set thresholds. In the event of communication failure, data is temporarily stored in the relay device and sent after communication resumes to help prevent loss of history. Usage scenarios: - Monitoring direct current at disaster prevention bases and important facilities - Checking current values and history of direct circuits from emergency power supplies to load equipment - Confirming inspection targets and notification status before on-site visits Expected effects from implementation: - Comparing current trends before and after changes in time periods and operations - Consolidating measurement information from multiple circuits for review - Utilizing normal operation history as reference information for inspections and BCP verification We will propose configurations based on monitoring targets, number of circuits, cable diameters, and installation environments.

  • Ammeter
  • Data Logger
  • Power Monitoring Equipment
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Wastewater (Water Quality and Water Level) Monitoring System for the Chemical Industry

Streamlining wastewater management in chemical plants to reduce environmental impact.

In the chemical industry, there is a demand for compliance with environmental regulations and sustainable business operations. In particular, managing wastewater from factories is crucial for preventing water pollution and contributing to environmental conservation. It is necessary to accurately monitor the quality and level of wastewater and to detect abnormalities early in order to minimize environmental risks. Our wastewater (quality and level) monitoring system addresses these challenges. 【Use Cases】 - Wastewater tanks and drainage channels in chemical plants - Continuous monitoring of water quality and level - Automatic notification and response in case of abnormalities 【Benefits of Implementation】 - Increased efficiency in wastewater management - Reduced environmental risks - Compliance with regulations

  • Water quality testing
  • pH meter
  • Water quality improvement
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality and Level Monitoring System for Power Plants

Streamlining cooling water management at power plants, with automatic monitoring of water quality and water levels.

In the management of cooling water at power plants, proper management of water quality and water levels is essential for balancing stable equipment operation and environmental considerations. Abnormalities in cooling water can lead to decreased power generation efficiency and equipment failures. Additionally, exceeding discharge standards carries the risk of legal liability. Our wastewater monitoring system addresses these challenges by monitoring water quality and water levels in real-time and detecting abnormalities early. 【Usage Scenarios】 - Management of wastewater from cooling towers - Monitoring of wastewater treatment facilities - Management of cooling water for emergency generators 【Benefits of Implementation】 - Early detection of abnormalities in water quality and water levels to prevent equipment troubles - Reduction of risks associated with exceeding discharge standards - Labor-saving and reduction of management costs through remote monitoring

  • Water quality testing
  • pH meter
  • Water quality improvement
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Wastewater (Water Quality and Water Level) Monitoring System for Food Processing

Streamlining wastewater management in food processing to reduce the risk of foreign matter contamination.

In the food processing industry, foreign matter contamination during the manufacturing process is a serious issue that not only compromises product quality but also undermines corporate trust. Wastewater management is crucial for understanding the sanitary conditions of the manufacturing environment and reducing the risk of foreign matter contamination. By monitoring the quality and level of wastewater, abnormalities can be detected early, allowing for prompt responses. Our wastewater monitoring system contributes to the efficiency of wastewater management in food processing. 【Usage Scenarios】 - Food manufacturing plants - Wastewater treatment facilities - Processes with a high risk of foreign matter contamination 【Benefits of Implementation】 - Early detection of wastewater quality abnormalities - Reduction of foreign matter contamination risks - Strengthening of sanitary management in the manufacturing environment - Compliance with regulations

  • Water quality testing
  • pH meter
  • Water quality improvement
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Drainage (Water Quality and Water Level) Monitoring System for Mining Industry

Streamlining drainage management in mining to reduce environmental pollution risks.

In mining, water quality management of drainage is extremely important for environmental conservation. In particular, it is essential to prevent the leakage of harmful substances and minimize the impact on the surrounding environment. Abnormalities in water quality and water levels can lead to serious environmental pollution. Our drainage monitoring system allows for real-time monitoring of water quality and water levels, enabling quick responses by detecting anomalies early. 【Usage Scenarios】 - Locations where drainage occurs, such as mines, concentration plants, and smelters - Monitoring of wastewater treatment facilities - Compliance with environmental regulations 【Benefits of Implementation】 - Reduces the risk of water quality pollution - Contributes to environmental conservation - Ensures compliance with legal regulations
  • Water quality testing
  • pH meter
  • Water quality improvement
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Industrial Wastewater Treatment Monitoring System for Chemical Plants

Autonomous control of water quality measurement, valve opening and closing adjustment, and chemical dosing.

In the chemical plant industry, there is a demand for compliance with environmental regulations and improvement of operational efficiency. Particularly in wastewater treatment processes, thorough water quality management and maintenance of stable treatment capacity are crucial. Abnormal water quality or reduced treatment capacity can increase the risk of environmental pollution and operational shutdowns. Our industrial wastewater treatment monitoring system automates the measurement of water quality, water level, and flow rate, achieving optimal wastewater treatment through autonomous control. 【Usage Scenarios】 - Wastewater treatment tanks in chemical plants - Automation of water quality management - Optimization of valve operation and chemical dosing 【Benefits of Implementation】 - Early detection of anomalies through visualization of water quality data - Optimization of treatment capacity through autonomous control - Labor-saving through remote monitoring and operation

  • Water quality testing
  • valve
  • Water quality improvement
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Industrial wastewater treatment monitoring system for semiconductors

Autonomous control of water quality measurement, valve opening and closing adjustment, and chemical dosing.

In the semiconductor manufacturing industry, there is a demand for the efficient use of water resources in the manufacturing process and the optimization of wastewater treatment processes. In particular, advanced water quality management is essential in the semiconductor manufacturing process, and delays or deficiencies in wastewater treatment can lead to decreased production efficiency and environmental risks. Our industrial wastewater treatment monitoring system automates the measurement of water quality, water level, and flow rate, and achieves autonomous control such as valve adjustment and chemical dosing, contributing to the efficiency of the wastewater treatment process. 【Usage Scenarios】 - Wastewater treatment facilities in semiconductor manufacturing plants - Business efficiency improvement through automation of water quality management - Rapid response to abnormalities through remote monitoring 【Benefits of Implementation】 - Reduction of wastewater treatment costs through optimization of water quality management - Risk mitigation through rapid response to abnormal occurrences - Continuous improvement based on data

  • Water quality testing
  • valve
  • Water quality improvement
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Condensation Risk Monitoring System for Pharmaceuticals

Maintain the quality of pharmaceuticals! Monitor condensation risks and support prompt measures.

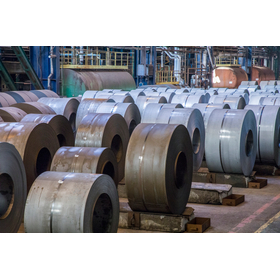
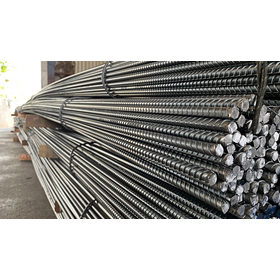
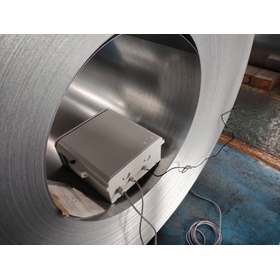
In the pharmaceutical industry, thorough management of storage environments is required to maintain product quality. In particular, condensation caused by changes in temperature and humidity poses a significant risk of degradation and quality deterioration of pharmaceuticals. Condensation can promote the decomposition of active ingredients and the deterioration of containers, potentially adversely affecting the safety and efficacy of the products. Our condensation risk monitoring system contributes to the preservation of pharmaceutical quality. 【Usage Scenarios】 - Pharmaceutical storage warehouses - Quality control in manufacturing processes - Areas where temperature and humidity management is critical 【Benefits of Implementation】 - Early detection and countermeasures for condensation risks - Preservation of pharmaceutical quality - Assurance of product safety - Optimization of storage environments

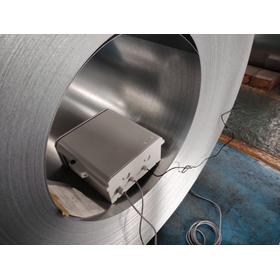
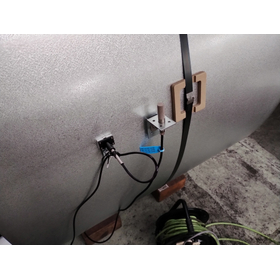
  • IMG_センサユニット.jpg
  • IMG_センサ設置状況.jpg
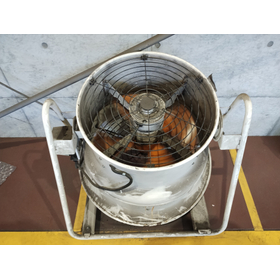
  • IMG_送風機.jpg
  • IMG_鋼板コイル.jpg
  • IMG_条鋼.jpg
  • Other information systems
  • Temperature and humidity measuring instruments
  • Other quality control systems
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Condensation Risk Monitoring System for Food Manufacturing

We monitor the risk of mold occurrence in food manufacturing to ensure quality.

In the food manufacturing industry, it is important to suppress the occurrence of mold in order to maintain product quality. Particularly in environments with high temperature and humidity, condensation is likely to occur, which can become a breeding ground for mold. Condensation can lead to product deterioration and unpleasant odors, potentially damaging a company's reputation. Our condensation risk monitoring system calculates the dew point temperature from the ambient temperature and humidity, and assesses the risk of condensation by monitoring the difference between the surface temperature of the monitored object and the dew point. By notifying via email, patrol lamps, or automated voice calls according to the risk level, we encourage prompt responses and suppress the occurrence of mold. 【Usage Scenarios】 - Food storage warehouses - Manufacturing lines - Refrigeration and freezing equipment - Product quality control 【Benefits of Implementation】 - Reduction of mold occurrence risk - Maintenance of product quality - Reduction of food waste - Gaining customer trust

  • IMG_センサユニット.jpg
  • IMG_センサ設置状況.jpg
  • IMG_送風機.jpg
  • IMG_鋼板コイル.jpg
  • IMG_条鋼.jpg
  • Other information systems
  • Temperature and humidity measuring instruments
  • Other quality control systems
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Automotive Condensation Risk Monitoring System

A condensation risk monitoring system that protects the quality of automotive parts.

In the automotive industry, maintaining the quality of parts is crucial. In particular, metal and electronic components are constantly exposed to the risk of deterioration due to rust and corrosion from condensation, as well as electrical system malfunctions. Condensation can lead to a decline in product performance and safety issues. Our condensation risk monitoring system calculates the dew point temperature from the ambient temperature and humidity, and determines the risk of condensation by monitoring the difference from the surface temperature of the monitored object. By notifying based on the risk level through email, patrol lamps, and automated voice calls, we encourage prompt responses and reduce the risk of component deterioration. 【Usage Scenarios】 - Storage locations for metal parts - Manufacturing processes for electronic components - Storage locations for finished vehicles - During the transportation of parts 【Benefits of Implementation】 - Maintenance of part quality - Reduction of defective products - Gaining customer trust - Cost reduction

  • IMG_センサユニット.jpg
  • IMG_センサ設置状況.jpg
  • IMG_送風機.jpg
  • IMG_鋼板コイル.jpg
  • IMG_条鋼.jpg
  • Other information systems
  • Temperature and humidity measuring instruments
  • Other quality control systems
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Groundwater Continuous Monitoring System for Mining

Cloud service for automating water quality management operations.

In the mining industry, managing the quality of wastewater is crucial to prevent environmental pollution caused by harmful substances contained in the discharge. In particular, groundwater contamination has a significant impact on the surrounding environment, necessitating appropriate monitoring and prompt responses. Implementing monitoring of groundwater quality and levels, along with information disclosure, is also important as part of a company's social responsibility. Our continuous groundwater monitoring system balances the efficiency of water quality management operations with contributions to environmental conservation. 【Usage Scenarios】 - Wastewater treatment facilities at mines - Groundwater monitoring in surrounding areas - Compliance with environmental regulations 【Benefits of Implementation】 - Early detection of water quality anomalies and rapid response - Increased efficiency in water quality management operations - Reduction of environmental risks

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Groundwater Continuous Monitoring System for Urban Development

Automating water quality management operations to reduce flooding risks.

In urban development, flood prevention measures are extremely important for ensuring the safety of the city. In recent years, there have been frequent flooding damages due to sudden heavy rains, and prompt responses are required. By continuously monitoring changes in groundwater levels and water quality, and detecting abnormalities early, it is possible to reduce flood risks and enhance urban safety. Our groundwater monitoring system contributes to this effort. 【Usage Scenarios】 - Management of groundwater in urban areas - Monitoring of rainwater retention facilities - Monitoring of areas with high flood risk 【Effects of Implementation】 - Early detection and response to flooding damage - Increased efficiency in groundwater management - Improved safety of the city

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Groundwater Continuous Monitoring System for Pharmaceuticals

Automating water quality management operations to support stable water supply assurance.

In the pharmaceutical industry, a stable supply of water for drug manufacturing is essential. Thorough water quality management is important for maintaining product quality, streamlining manufacturing processes, and ensuring compliance. While the use of groundwater can lead to cost reductions, it also requires rapid responses to fluctuations in water quality and levels, as well as to emergencies. Our groundwater constant monitoring system addresses these challenges and supports the secure supply of stable water. 【Usage Scenarios】 - Monitoring of water for drug manufacturing - Continuous monitoring of water quality and levels in groundwater use - Rapid response to water quality anomalies 【Benefits of Implementation】 - Reduction of quality risks through early detection and response to water quality anomalies - Cost optimization in groundwater use - Streamlining and labor-saving in water quality management operations

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Management System (Turbidity) for Pharmaceuticals

Cloud service for automating water quality management operations.

In the pharmaceutical industry, managing the water quality of pure water in the manufacturing process is crucial to ensure product quality. In particular, constant monitoring of water quality is required to prevent contamination and microbial growth. High turbidity can lead to a decline in product quality and issues in the manufacturing process. Our water quality management system measures turbidity and contributes to the efficiency of water quality management operations. 【Usage Scenarios】 - Turbidity monitoring in the pure water manufacturing process - Quality management of manufacturing water - Monitoring of cleaning water 【Benefits of Implementation】 - Reduction of quality risks through early detection of water quality abnormalities - Increased efficiency of water quality management operations - Maintenance of stable product quality

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Waterworks Bureau

Utilizing water quality data to streamline leak detection.

The waterworks bureau requires rapid leak detection to minimize losses due to water leaks. Abnormal water quality may indicate signs of leaks, making early detection crucial. This system contributes to improving the accuracy of leak detection by monitoring turbidity, color, and residual chlorine data in real-time and detecting anomalies. 【Usage Scenarios】 - Detection of abnormalities in water pipes - Visualization of water quality data - Remote monitoring 【Benefits of Implementation】 - Reduction of leak risks - Increased efficiency in water quality management operations - Minimization of damage through prompt response

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Food Manufacturing

Automate water quality management operations and streamline quality control.

In the food manufacturing industry, managing the water quality used in production is crucial for maintaining product quality. In particular, proper management of turbidity, color, and residual chlorine is essential to ensure product safety and quality. When water quality deviates from standard values, it can lead to discoloration, off-odors, and spoilage of products, potentially resulting in customer complaints and product disposal. Our water quality monitoring system contributes to the efficiency of quality management by monitoring these water quality parameters in real-time and detecting anomalies early. 【Usage Scenarios】 - Water quality management in food manufacturing plants - Water quality management in beverage production - Water quality management in food processing 【Benefits of Implementation】 - Maintenance of product quality through early detection of water quality anomalies - Streamlining of water quality management operations - Realization of quality improvement based on data

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Beverage Manufacturing

Automate water quality management and reduce the risk of foreign substance contamination.

In the beverage manufacturing industry, thorough management of the water used in production is essential to ensure product quality and safety. In particular, foreign matter contamination is a serious issue that can lead to product quality deterioration and health hazards for consumers. Strict water quality management is crucial to minimize these risks. Our water quality monitoring system continuously monitors turbidity, color, and residual chlorine in real-time, allowing for the early detection of abnormalities and reducing the risk of foreign matter contamination. 【Usage Scenarios】 - Water quality management in the beverage manufacturing process - Monitoring of source water, manufacturing water, and cleaning water - Early detection of foreign matter contamination risks 【Benefits of Implementation】 - Improved product quality through early detection of water quality abnormalities - Reduced risk of foreign matter contamination - Increased efficiency in water quality management operations

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Power Plants

Automating cooling water management to support stable operation.

In the management of cooling water at power plants, ensuring the efficient operation of equipment and safety is crucial. The quality of cooling water affects equipment corrosion and scale buildup, leading to decreased power generation efficiency and potential failures. In particular, proper management of turbidity, color, and residual chlorine is essential for the stable operation of the cooling water system. This system monitors these water quality parameters in real-time and detects abnormalities early, preventing equipment troubles before they occur. 【Usage Scenarios】 - Cooling water systems such as cooling towers and heat exchangers - Automation of water quality management - Early detection of water quality abnormalities 【Benefits of Implementation】 - Stable operation of equipment - Reduction of maintenance costs - Increased efficiency in water quality management tasks

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Hydropower Generation

Monitor cooling water quality to reduce environmental impact and improve power generation efficiency.

In the hydropower generation industry, there is a demand for consideration of the environment and improvement of power generation efficiency. The quality of cooling water affects equipment corrosion and scale buildup, leading to decreased power generation efficiency and equipment failures. In particular, proper management of turbidity, color, and residual chlorine is essential for environmental conservation and stable operation. This system monitors these water quality parameters in real-time and detects anomalies early, thereby reducing environmental impact and preventing equipment troubles. 【Usage Scenarios】 - Cooling water systems such as cooling towers and heat exchangers - Automation of water quality management - Early detection of water quality anomalies 【Benefits of Implementation】 - Stable operation of equipment - Reduction of maintenance costs - Increased efficiency in water quality management tasks

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Geothermal Power Generation

Automate cooling water management to support the efficient operation of geothermal resources.

In geothermal power generation, the effective utilization of geothermal resources and the stable operation of power generation equipment are crucial. The quality of cooling water affects equipment corrosion and scale deposition, leading to decreased power generation efficiency and potential failures. In particular, proper management of turbidity, color, and residual chlorine is essential for the stable operation of the cooling water system. This system monitors these water quality parameters in real-time and detects anomalies early, preventing equipment troubles and supporting the efficient operation of geothermal resources. 【Usage Scenarios】 - Cooling water systems such as cooling towers and heat exchangers - Automation of water quality management - Early detection of water quality anomalies 【Benefits of Implementation】 - Stable operation of equipment - Reduction of maintenance costs - Increased efficiency in water quality management tasks

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Steelmaking

Automate cooling water management to suppress equipment corrosion.

In the steel industry, suppressing corrosion caused by cooling water is crucial for stable equipment operation and maintaining product quality. The quality of cooling water affects equipment corrosion and scale deposition, which can lead to equipment failures and a decline in product quality. In particular, proper management of turbidity, color, and residual chlorine is essential for the stable operation of cooling water systems. This system monitors these water quality parameters in real-time and detects anomalies early, preventing equipment troubles and suppressing corrosion. 【Usage Scenarios】 - Cooling water systems such as cooling towers and heat exchangers - Automation of water quality management - Early detection of water quality anomalies 【Benefits of Implementation】 - Stable equipment operation - Reduction of maintenance costs - Maintenance of product quality

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Food Manufacturing

Automating water quality management in food manufacturing.

In the food manufacturing industry, managing the quality of water used is crucial to ensure product quality and safety. In particular, the water used in the manufacturing process not only directly affects the taste and quality of the product but also needs to manage the risks of foreign substance contamination and bacterial growth. By properly managing water quality parameters such as turbidity, color, and residual chlorine, the risks of product quality deterioration and food poisoning can be reduced. This system monitors these water quality parameters in real-time and ensures food safety by detecting abnormalities early. 【Usage Scenarios】 - Food manufacturing lines - Cleaning processes - Cooling water systems 【Benefits of Implementation】 - Improved product quality - Reduced risk of food poisoning - Increased efficiency in water quality management tasks

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Water Quality Monitoring System for Semiconductor Manufacturing

Real-time monitoring of ultrapure water quality to stabilize its quality.

In the semiconductor manufacturing industry, the management of ultrapure water quality, which affects product quality, is crucial. In particular, the contamination of impurities can adversely impact the manufacturing process, leading to reduced yield and product defects. This system monitors the turbidity, color, and residual chlorine of ultrapure water in real-time, enabling early detection of anomalies and supporting the production of high-quality products. 【Application Scenarios】 - Ultrapure water manufacturing process - Pure water supply line - Automation of water quality management 【Benefits of Implementation】 - Improvement in product quality - Enhancement of yield - Stabilization of the manufacturing process

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Machine Vibration Monitoring System for Manufacturing Industry

Monitor the vibrations of industrial machinery to reduce unplanned downtime.

In the manufacturing industry, the stable operation of equipment affects production efficiency. Unexpected machine failures can lead to production line stoppages, resulting in significant losses. It is important to detect abnormalities caused by vibrations early and to carry out planned maintenance to minimize downtime. Our machine vibration monitoring system monitors vibration data from industrial machinery in real-time and detects abnormalities to prevent equipment failures before they occur. 【Use Cases】 - Abnormality detection of machine tools and conveyor equipment on the production line - Monitoring of plant equipment operating 24 hours a day - Understanding the status of equipment located in remote areas 【Benefits of Implementation】 - Reducing the risk of production stoppages due to sudden machine failures - Cost reduction through planned maintenance - Extending the lifespan of equipment - Labor savings through remote monitoring

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Vibration Monitoring System for Chemical Plants

Monitoring the vibrations of plant equipment to support safe operations.

In the chemical plant industry, the safe operation of equipment is the most important issue. In particular, abnormal vibrations in rotating machinery can lead to serious accidents. Vibration monitoring systems are essential for improving the safety of the plant. 【Usage Scenarios】 * Rotating machinery such as reactors, pumps, and compressors * Plants handling hazardous materials * Plants operating continuously 24 hours a day 【Benefits of Implementation】 * Early detection of equipment abnormalities to prevent accidents * Reduction of downtime through planned maintenance * Improvement of overall plant safety

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Machine Vibration Monitoring System for the Food Manufacturing Industry

Reduce the risk of foreign matter contamination in food manufacturing lines and strengthen quality control.

In the food manufacturing industry, foreign object contamination is a serious issue that not only undermines product quality and safety but can also damage a company's reputation. Abnormal vibrations in machinery on the production line are one sign of potential contamination, making early detection and countermeasures essential. Our machine vibration monitoring system continuously monitors the vibrations of key machinery on the production line in real-time, detecting anomalies to reduce the risk of foreign object contamination and ensure food safety. 【Use Cases】 - Machinery such as filling machines, packaging machines, and conveyors in food manufacturing lines - Processes with a high risk of foreign object contamination 【Benefits of Implementation】 - Early detection of machinery abnormalities to prevent foreign object contamination - Improvement in product quality and safety - Enhanced company reliability

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Machine Vibration Monitoring System for Automotive Manufacturing

Reduce production line downtime and improve operational efficiency.

In the automotive manufacturing industry, production line stoppages lead to significant losses. In particular, failures of key equipment such as press machines and welding robots can impact the entire production schedule, potentially resulting in delivery delays and loss of customer trust. A machine vibration monitoring system aims to address these challenges by early detection of equipment anomalies and preventing line stoppages before they occur. 【Usage Scenarios】 * Press machines * Welding robots * Conveyor systems * Painting lines 【Benefits of Implementation】 * Reduction in unexpected line stoppages * Cost optimization through planned maintenance * Improvement in production efficiency * Stabilization of quality

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

[For the Energy Industry] IoT Sensor Integration Automated Voice Dialing Service

Notification of abnormalities from the remote monitoring system via automated voice call.

In the energy industry's remote monitoring systems, it is crucial to quickly detect and respond to equipment abnormalities and emergencies. Particularly in critical infrastructure such as power plants and substations, early detection of anomalies leads to the prevention of accidents and a reduction in recovery time. Rapidly communicating the occurrence of abnormalities to the responsible personnel is an important challenge in remote monitoring. Our IoT sensor-linked automatic voice calling service works in conjunction with M2MSTREAM to automatically make voice calls when an anomaly is detected, enabling swift information transmission to the responsible personnel. 【Use Cases】 - Detection of equipment abnormalities in power plants and substations - Detection of abnormalities in oil and gas plants - Remote monitoring of renewable energy facilities 【Benefits of Implementation】 - Accelerated initial response during abnormal occurrences - Reduction of human errors - Strengthened monitoring system available 24/7, 365 days a year

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Digital Transformation of Wastewater Treatment for Pharmaceuticals using IoT/AI

Supporting quality control in pharmaceutical factories through the digital transformation of wastewater treatment.
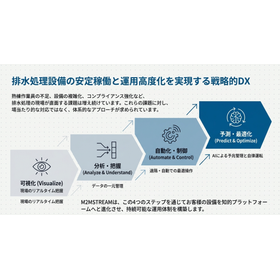
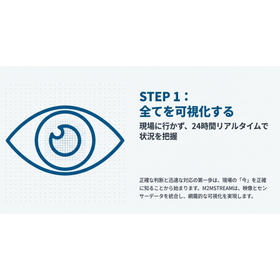
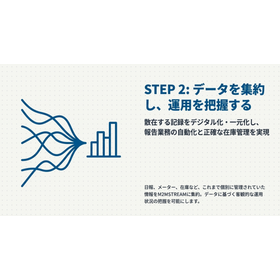
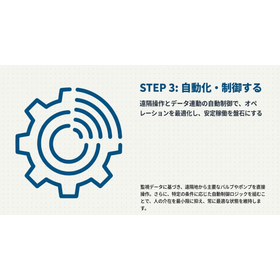
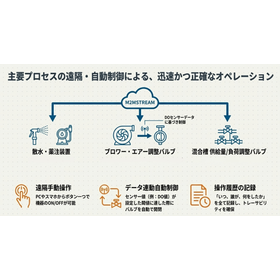
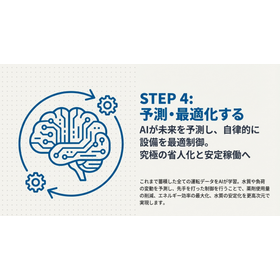
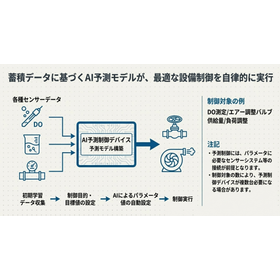
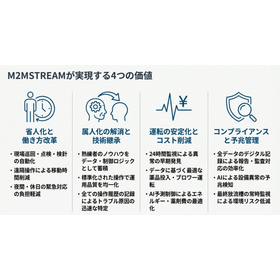
In the pharmaceutical industry, strict management of water quality in the manufacturing process is required. The quality of wastewater treatment directly affects the quality of the products, so it is important to maintain a consistently stable water quality. Manual water quality management carries risks due to human error and delays in measurement. Our IoT/AI-based wastewater treatment digital transformation system automates water quality monitoring, scum recovery, automatic dosing of sludge settling agents, and streamlines chemical inventory management, contributing to improved quality control. 【Usage Scenarios】 - Wastewater treatment facilities in pharmaceutical factories - Streamlining water quality management - Strengthening quality control 【Benefits of Implementation】 - Real-time monitoring of water quality data - Optimization of chemical usage - Reduction of on-site workload
  • 排水DXスライド1.png
  • 排水DXスライド2.png
  • 排水DXスライド3.png
  • 排水DXスライド4.png
  • 排水DXスライド5.png
  • 排水DXスライド6.png
  • 排水DXスライド7.png
  • 排水DXスライド8.png
  • Wastewater/wastewater treatment equipment
  • Other water supply and drainage facilities
  • Wastewater treatment equipment, technology and maintenance
  • Surveillance system

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration