
Design of operational data to track chocolate stops and construction of production lines | Termix

Not just a line that doesn't stop, but a line that can trace the reasons for stopping.
We do not know the cause of the chocolate stop, and we face the challenge of being unable to trace the relationship between inspection failures and previous processes. To address this, we design a production line that retains three types of operational data—stop, production, and quality—in a form that can be used for decision-making on-site. We combine the perspectives of equipment manufacturers, FA integrators, and line builders, providing consistent support from conceptual design to control design and HMI design. Operational data is not added externally later; instead, it is integrated with the design of PLC abnormal conditions and codes, as well as the design of HMI display and history screens, determining who will use which data. We specialize in designing operational data and the overall production line, covering everything from transportation, inspection, control, maintenance, to on-site operations. "Unable to identify the cause of chocolate stops" → Reduce investigation time for causes through the design of stop history granularity. "I want to trace the relationship between inspection failures and previous processes" → Record related to product type, lot, and process history. "I want to reduce the cause investigation time for maintenance personnel" → Display abnormal history and recovery procedures on the HMI. "I want to reduce defects immediately after setup changes" → Correlate product change conditions with inspection results. "I want to modify existing lines to collect data" → Review from control design and HMI design. For inquiries about how to proceed with operational data design or its application scope, please contact us for document requests or technical consultations.
Inquire About This Product
basic information
**Functions and Features** - Stoppage Data: Process name, details of the anomaly, occurrence time, recovery time, product type, equipment status - Confirmation of sensor status just before stoppage, presence of workpieces, and interlock status - Production Data: Production count, OK count, NG count, takt time, cycle time, product type, lot - Quality Data: Inspection results, measurement values, NG items, image inspection judgments, presence of re-inspection - Distinction between automatic recovery and human intervention, recording of time taken for recovery **Implementation Effects** If the stoppage display only indicates "abnormal stoppage," the investigation of the cause relies on human memory and experience. By categorizing anomalies down to the process unit and making visible not only anomalies with long stoppage times but also those with high occurrence rates, we can lead to reduced recovery times, improved maintainability, quality enhancement, and stabilized operations. **Features** - Causes are differentiated across the entire line connecting robots, conveyors, inspection devices, processing machines, supply devices, and existing equipment. - The waiting for workpieces in the conveyance process is traced back to the discharge timing of the previous process and the acceptance conditions of the subsequent process. - Inspection NGs are verified in relation to workpiece posture, tool wear, and vibrations during transport. - During the conceptual stage, we organize "what we want to track later" and determine the granularity of records according to product characteristics and quality requirements.
Price range
Delivery Time
Applications/Examples of results
Corresponding processes: supply, transportation, extraction, jig setup, processing, assembly, inspection, and dispatch to the next process Corresponding forms: automated lines, labor-saving lines, modifications and connections to existing lines Scope of provision: from conceptual design, equipment design, control design, and HMI design to design considering maintenance and on-site operations Target departments: production technology department, manufacturing department, maintenance department, quality control department Consideration stage: conceptualization of new lines, operational improvements after equipment installation, additional data collection for existing lines Aggregation units: confirmation of occurrence trends by process, product type, lot, and time zone Implementation purposes: measures against chocolate stops, visualization of abnormal history, ensuring traceability in inspection processes, extraction of improvement themes
catalog(1)
Download All Catalogs
Company information
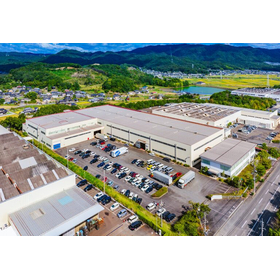
We, Thermix, a top-tier production line builder with proven expertise, handles automation and line construction for production equipment across diverse fields including automobiles and automotive parts, aircraft bodies, and industrial machinery. We provide full turnkey solutions from concept and specification review through design, manufacturing, installation, commissioning, and maintenance, ensuring reliable mass production launch. Leveraging our production technology expertise, we organize and visualize the current state, including process feasibility, integration with existing equipment, and safety. Utilizing industrial robots, image processing, conveyance/inter-process transfer, and material handling, we propose realistic automation roadmaps without unnecessary strain. We address challenges like “We want to reduce staffing on lines that can't be stopped” or “Equipment investment decisions are difficult,” accompanying you from small-scale PoCs to full-scale deployment with our project management expertise. Leveraging our domestic and international launch experience, we collaborate to create the optimal production line.
