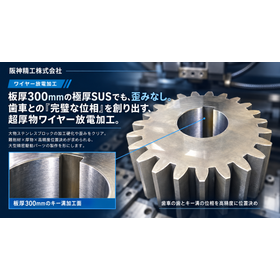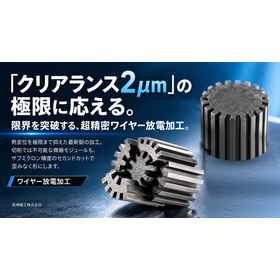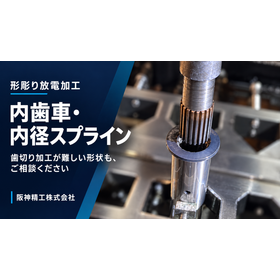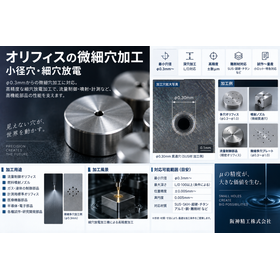

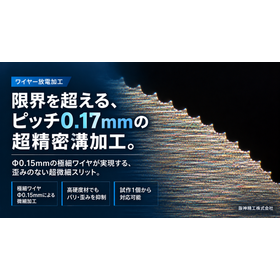
Case study of continuous groove machining with φ0.15mm wire and a pitch of 0.17mm. We will consider discharge conditions, fluid pressure, and machining sequence taking into account the thin-walled shape.
At Hanshin Seiko, we accept consultations for machining fine grooves, fine slits, and narrow pitch shapes using wire cut electrical discharge machining. The case presented involves continuous fine groove machining with a pitch of 0.17mm between the centers of grooves, using a φ0.15mm wire electrode. In the case of fine continuous grooves, it is necessary to consider not only the formation of the grooves but also the thin sections left between them. We take into account the wire diameter and discharge gap to determine the machining width, as well as the discharge energy, machining cost, fluid pressure, and machining sequence. We will confirm the material, plate thickness, groove width, pitch, required tolerances, and necessary remaining thickness dimensions, and provide guidance on the appropriate machining methods based on the shape. Please feel free to consult us about fine parts with comb-like or multi-groove shapes that you may be struggling to process. Based in Kobe City, Hyogo Prefecture, we respond to inquiries from across the country. Please provide us with your drawings, quantities, and desired delivery dates.
Inquire About This Product
basic information
【Processing Conditions for Published Examples】 Processing Method: Wire Cut Electrical Discharge Machining Wire Diameter: φ0.15mm Pitch Between Groove Centers: 0.17mm Processing Shape: Continuous Fine Grooves Considerations: Groove Width, Remaining Material Dimensions, Discharge Conditions, Processing Liquid Pressure, Processing Sequence, Wire Path *0.17mm refers to the center-to-center distance between adjacent grooves, not the groove width. The wire diameter differs from the actual groove width. *The final groove width, remaining material dimensions, material, plate thickness, and tolerance measurements are not shown in this publication. Availability and accuracy will be confirmed by checking the drawings and processing conditions.
Price information
This is an individual estimate for each drawing. We will confirm the material, plate thickness, groove width, pitch, number and length of grooves, required tolerances, remaining material dimensions, and quantity to provide the estimate.
Delivery Time
※We will check the drawings, quantities, setup conditions, and equipment operating status, and provide individual guidance. Please let us know the planned delivery date for materials and parts, as well as your desired delivery date.
Applications/Examples of results
【Case Study】 Continuous fine groove processing with a wire electrode of φ0.15mm and a center-to-center pitch of 0.17mm. 【Shapes and Challenges We Can Consult On】 - Fine continuous grooves and slits - Parts with grooves arranged at narrow pitches - Shapes that leave thin sections between grooves - Precision parts with comb-like and multi-groove shapes - Processing that requires consideration for deformation or damage to thin sections - Fine shapes that are difficult to handle with conventional processing methods The feasibility of processing will be considered based on material, plate thickness, groove width, pitch, tolerance, and required remaining thickness dimensions. *This is not a sale of standard products, but a contract processing service based on drawings.
Company information

Hansei Seiko Co., Ltd. is a precision metal processing company founded in 1948, based in Kobe City, Hyogo Prefecture. We offer integrated processing services centered around wire cut electrical discharge machining, shape electrical discharge machining, and fine hole electrical discharge machining, as well as machining, polishing, finishing, and measurement. We welcome inquiries for precision parts, mold components, jigs, test pieces, and more, whether for single items, prototypes, or small lots. In addition to processing hardened steel, carbide, and stainless steel, we also handle contour machining of thick parts, key grooves, fine slits, and complex shapes. We confirm material, shape, required precision, and application, and consider processing conditions and processes. This reduces the burden of arranging multiple processing locations and supports part manufacturing. Based on the principle of "making according to the drawings," we conduct inspections and measurements in-house to confirm the finish before shipping. Based in Kobe and Hyogo, we accept processing inquiries and quotation requests from across the country. If you have parts you are struggling to process or drawings for which you would like to consider methods and processes, please feel free to consult with us. https://www.hansei.co.jp/