Casting Simulation | Pre-check of Molten Flow and Solidification for Aluminum Casting Prototyping
AC4CH/AC4C/AC2A/AC7A/AC8B and other 10 aluminum alloys and 8 copper alloys.

Defects such as casting voids and poor flow in the trial castings have occurred, leading to continuous rework. Before casting, we analyze the flow and solidification, and we can ship prototypes in as little as two weeks from a single piece.
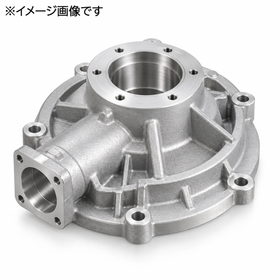
When I received the trial casting, I found that there were casting defects on the machined surface. The molten metal did not fully flow into the thin areas. Each time we correct the mold and recast, the evaluation schedule gets pushed back. This is a common vicious cycle that occurs during the launch of new parts. Many defects in castings are determined by how the molten metal flows within the mold and the order in which it solidifies. If the positions of the pouring gate and riser do not match the shape, shrinkage tends to accumulate in the areas that solidify last, while in the thin sections, the metal solidifies before it can reach them. Karmo Casting decides on the plan after confirming the flow of molten metal and solidification through casting simulations. Since the wooden molds are designed and manufactured in-house, the results of the analysis can be directly reflected in the placement of the pouring gate and riser as well as the shape of the mold. We handle everything in-house, from casting to machining and inspection using a three-dimensional measuring machine, starting from a single prototype. The results of the analysis also help identify areas where the design should be reconsidered, such as parts with significant differences in wall thickness. We are offering a guidebook summarizing the causes and countermeasures for casting defects, poor metal flow, and cracking for free.
Inquire About This Product
Related Videos
basic information
【Analysis】Preliminary plan examination using casting simulation (flow and solidification) 【Supported Lot】From 1 piece 【Prototype Delivery Time】As short as 2 weeks 【Casting Size】50mm square to 1,000mm square / Minimum thickness 1mm (local) / 1.5mm (overall) 【Supported Materials】 - Aluminum Alloys: AC2A / AC2B / AC3A / AC4A / AC4B / AC4C / AC4CH / AC4D / AC7A / AC8B - Copper Alloys: CAC403 / 406 / 502 / 301 / 302 / 303 / 702 / 703 【Casting Process】In-house capabilities for 5 methods: sand mold / self-hardening / alkaline phenolic / cold box / metal mold 【Processing Equipment】15 units of 5-axis machining centers / 2 gantry type / 3 vertical type / 2 NC lathes 【Processing Accuracy】Geometric tolerance ±0.03mm 【Inspection Equipment】2 contact-type 3D measuring machines / non-contact 3D digitizer (deviation 30-80μm) 【Certifications】ISO9001 (2012) / JIS Q 9100 (2015) / KEMS Step2 【Heat Treatment】T6 and others available
Price information
If you provide the drawings (along with 3D data if available) and the material and quantity, we will offer a free estimate along with the consideration of the plan. Reducing the need for rework through prior analysis helps to control the overall costs and schedule of the prototype. It also makes it easier to reduce processing costs. If the required quantity is five or more, we will also provide the costs for replacing it with casting.
Delivery Time
P4
※The prototype will be shipped in a minimum of 2 weeks, and the initial order, which includes the production of wooden molds, will take at least 3 weeks. The timeline may vary depending on the shape, material, and quantity, so please let us know the evaluation schedule.
Applications/Examples of results
【Industries Served】Automotive/CASE, Railways, Industrial Machinery, Power/Energy, Semiconductor Manufacturing Equipment, Marine Vessels 【Related Achievements】 ■ Countermeasures for casting defects in pressure-resistant components (stopping leaks with casting plans and CAE analysis) ■ Cylinder cases for railway vehicles (AC4CH-T6 / complex shape with 6 cores) ■ Industrial machinery parts (AC4CH-T6 / complex shape with 11 cores) 【Used in Such Situations】 - Casting defects and poor flow occur with every prototype - Concerns about defects due to a mix of thin and thick areas - Evaluation schedule is set, and there is no room for rework - First-time casting of components requiring pressure resistance and airtightness - Want to identify areas needing shape review before prototyping 【Achievement Scale】200 companies and 5,000 items in the last 5 years. Over 500 prototype and development achievements annually.
catalog(2)
Download All Catalogs
Company information

At Karmo Casting Co., Ltd., we engage in aluminum processing, aluminum casting, and the casting of copper alloys other than aluminum. Manufacturing has continuously supported the backbone of Japanese industry. At Karmo Casting, we have maintained that spirit and pride, dedicating ourselves to pioneering initiatives in the industry since our founding. Our primary goal is to build partnerships with our customers. To achieve this, we believe it is essential to flexibly adapt to changes in the times and realize all kinds of needs. Our relentless pursuit of technical expertise, responsiveness, quality, and speed reflects this attitude. While sensitively and swiftly understanding our customers' thoughts, Karmo Casting will continue to accumulate tireless efforts and changes as a manufacturing company that is chosen and needed by our customers.