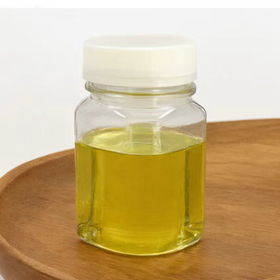
Natural red pigment derived from Monascus, red yeast extract anthocyanin-based coloring.
Monascus Red Color (Natural pigment derived from red yeast rice / Food additive grade - powder / liquid type)
60,000 mu cultivation base × international certification. Safe, stable, and high color development natural pigment derived from red yeast rice. Widely applicable to beverages, confections, dairy products, and processed foods.
This product, "Monascus Red Color," is a natural red coloring agent extracted from the red yeast fungus (Monascus purpureus). As a plant-based and microbe-derived food-compatible colorant, it achieves stable coloration ranging from vibrant red to orange. It is available in both powder and liquid forms, is highly water-soluble, and is suitable for a wide range of food applications, including beverages, confections, dairy products, and fermented foods. We own and operate our own cultivation bases and contract farming areas equivalent to approximately 60,000 mu, ensuring no pesticide use, contamination management, and strict quality selection. This allows us to provide high-quality red yeast consistently from the raw material stage. Our manufacturing complies with international standards, having obtained various certifications including ISO9001, FSSC22000, FDA registration, organic certification, HALAL, and Kosher. Our quality management system is widely adopted in OEM/ODM projects by domestic and international beverage manufacturers, confectionery makers, and dairy producers. As a naturally derived colorant, Monascus Red Color is also an ideal alternative to synthetic colorants. Additionally, it can be utilized in the development of clean label and organic products, combining color stability with safety.

Inquire About This Product
basic information
Product Name: Red Yeast Extract (Anthocyanin-based Natural Colorant) Scientific Name/Source: Extract derived from Monascus purpureus (Red Yeast) Form: Powder (Dried Powder) / Liquid (Concentrated Extract) Color: Red to Orange (Stable under acidic and neutral conditions) Solubility: Water-soluble (Stable under acidic conditions pH 2-6) Resistance: Excellent heat, light, and acid resistance Main Components: Monascus pigments (Monacolin, Anthocyanin-based) Quality Control: Heavy metal testing, pesticide residue testing, microbiological testing (Compliant with food standards) Raw Material Cultivation: Contract cultivation (Uncontaminated, pesticide management, variety management) Packaging: Powder 1kg/5kg/20kg aluminum bags, Liquid 20kg/200kg drums Storage Method: Recommended to store in a light-proof and low-temperature environment Lot Management: COA (Certificate of Analysis) available
Price range
Delivery Time
Applications/Examples of results
Food and Beverage Coloring for soft drinks, fermented beverages, and RTD drinks Confectionery applications such as jelly, gummies, and candies Coloring for yogurt, fermented milk, and dairy beverages Coloring for processed foods, noodles, and seasonings Health Foods and Supplements Coloring for powder supplements, smoothie mixes, and protein powders Differentiating materials for natural supplements and beauty foods OEM and International Market Extensive adoption by domestic and international beverage, confectionery, and dairy manufacturers Stable supply system through self-cultivated raw materials and internationally certified factories Benefits and Selling Points Food coloring derived from natural and microbial sources, ensuring safety High traceability and quality stability Stable coloration in acidic and neutral foods Ideal for clean label and organic products
Company information
Our company is a global raw material and technology solution provider that offers natural-derived ingredients, including herbal medicines and plant-derived extracts, as well as high value-added functional ingredient formulation technologies. We integrate knowledge of traditional natural materials with modern biotechnology and formulation techniques to cater to a wide range of fields, including pharmaceuticals, health foods, functional foods and beverages, cosmetics, personal care, and animal nutrition. Utilizing advanced technologies such as Cocrystal, Liposomal, microencapsulation, particle technology, pellet technology, and granulation technology, we provide customized solutions to address challenges related to the solubility, absorption, stability, flavor, and processability of functional ingredients. Additionally, we supply a diverse range of natural and functional ingredients, including plant extracts, natural flavors, essential oils, amino acids, and peptides. We have established a consistent global supply system that covers raw material procurement, processing, quality control, and export, allowing us to flexibly respond to development projects from small batches to mass production. Through high-quality raw materials, advanced technologies, and specialized support, we assist customers worldwide in product development and business expansion.