Natural Algal Oil Omega-3 Microcapsule Powder 1%・5%・10%
Microalgae-derived natural algal oil omega-3 microencapsulated powder (solvent-extracted, water-dispersible, soft capsule, suitable for beverages and dairy products)
Natural omega-3 fatty acids derived from microalgae. Improved oxidation stability through microencapsulation, ideal for soft capsules, beverages, and dairy products in a water-dispersible form.
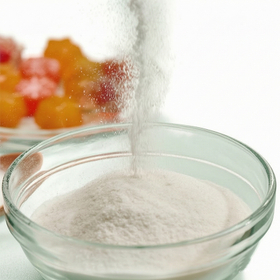
This product is a powdered raw material stabilized by microencapsulation (micronization) after obtaining high-purity omega-3 fatty acids (EPA and DHA) from the microalga Schizochytrium sp. (micro spherical algae) using food-grade solvent extraction. Microencapsulation significantly improves resistance to oxidation, light, and heat, enhancing the retention rate of components during long-term storage and product processing. This product is designed as a water-dispersible powder that disperses uniformly when added to cold water, with minimal sedimentation or aggregation. Therefore, it can be applied to a wide range of products, including hard capsules, tablets, solid beverages, jellies, gummies, energy bars, and dairy products. Additionally, it has high tabletability, making it stable for use in tablet products. Our omega-3 raw materials are exported to over 50 countries, including the United States, Japan, and Germany, and have been adopted by major companies in the pharmaceutical, cosmetics, and health food industries for many years. Our manufacturing facilities have obtained international certifications such as ISO9001, HALAL, Kosher, FDA, and RMP, ensuring safety, stable supply, and high quality.
Inquire About This Product
basic information
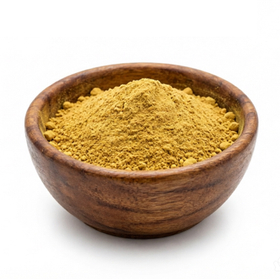
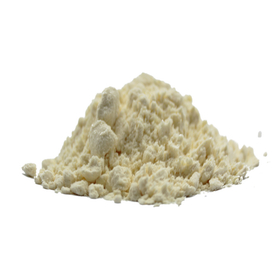
Ingredient Name: Natural Algal Oil Omega-3 Microcapsule Powder Composition Standards: Omega-3 Fatty Acids 1%, 5%, 10% (EPA and DHA content) Source: Microalgae Schizochytrium sp. Extraction Method: Food-grade solvent extraction (high purity, no residual solvents) Processing Technology: Microencapsulation (oxidation stabilization, microparticulation) Appearance: Light yellow to light orange fine powder Dispersion: Cold water dispersibility (uniform dispersion in water) Stability: Improved oxidation resistance, light resistance, and heat resistance Processing Suitability: 1. Ideal for incorporation into hard capsules, tablets, solid beverages, gummies, jellies, and dairy products 2. Uniform dispersion with minimal sedimentation and color variation 3. Stable even in low pH beverages Safety and Certification: ISO9001, HALAL, Kosher, FDA, RMP Passed heavy metal and microbiological testing Packaging: 1kg / 5kg / 20kg (OEM available) Export Record: Over 50 countries (including the USA, Japan, EU, Southeast Asia, etc.)
Price range
Delivery Time
Applications/Examples of results
■ Food and Beverage Applications 1. Soft drinks, functional drinks 2. Solid beverages, powdered sticks 3. Gummies, jelly 4. Dairy products (yogurt, fermented milk, plant-based milk) Energy bars, nutrition bars ■ Supplement Applications 1. Hard capsules 2. Tablets (with tablet resistance) 3. Beauty and health supplements 4. Cardiovascular support products 5. Brain function support supplements ■ Expected Health Functions 1. Improvement of blood lipids, cardiovascular health support 2. Anti-inflammatory effects 3. Maintenance of brain and nerve function 4. Lifestyle support 5. Enhancement of added value for supplements and functional foods ■ Implementation Results Adopted by pharmaceutical companies, health food OEMs, and dairy and beverage manufacturers, primarily in the U.S., Japan, and the EU. High evaluations for oxidation stability and water dispersibility through microencapsulation have led to its use in the development of diverse products such as hard capsules, tablets, beverages, dairy products, jelly, and gummies.
Company information
Our company is a global raw material and technology solution provider that offers natural-derived ingredients, including herbal medicines and plant-derived extracts, as well as high value-added functional ingredient formulation technologies. We integrate knowledge of traditional natural materials with modern biotechnology and formulation techniques to cater to a wide range of fields, including pharmaceuticals, health foods, functional foods and beverages, cosmetics, personal care, and animal nutrition. Utilizing advanced technologies such as Cocrystal, Liposomal, microencapsulation, particle technology, pellet technology, and granulation technology, we provide customized solutions to address challenges related to the solubility, absorption, stability, flavor, and processability of functional ingredients. Additionally, we supply a diverse range of natural and functional ingredients, including plant extracts, natural flavors, essential oils, amino acids, and peptides. We have established a consistent global supply system that covers raw material procurement, processing, quality control, and export, allowing us to flexibly respond to development projects from small batches to mass production. Through high-quality raw materials, advanced technologies, and specialized support, we assist customers worldwide in product development and business expansion.