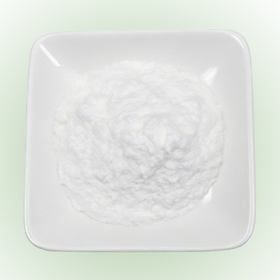
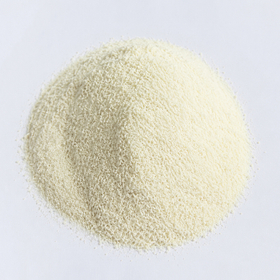
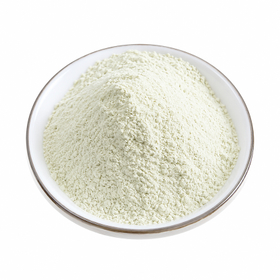
Natural black tea-derived brown pigment (Black Tea Brown water-soluble)
Black Tea Brown Color (Natural black tea extract / Water-soluble powder / Brown powder / Suitable for food, beverages, confections, and dairy products / Safe and stable)
Natural black tea-derived brown powder pigment. It is water-soluble, has high coloring power, and has little impact on flavor, making it ideal for a wide range of applications such as confectionery, beverages, dairy products, and frozen foods.
This product, "Black Tea Brown Color," is a natural edible colorant derived from the extraction and concentration of natural black tea (Camellia sinensis), resulting in a brown powder obtained through processes such as spray drying. It is purely natural, has a vibrant brown hue, excellent coloring power, and minimal impact on flavor. It easily dissolves in water but is insoluble in fats and ethanol. In the food sector, it is suitable for coloring frozen foods, confectionery, dairy products, chocolate, sugar-free foods, canned fish, and canned meat, and in the pharmaceutical field, it can also be applied to sugar-coated tablets and pharmaceutical coatings. Additionally, it can be used in ice cream and beverages, allowing for a wide range of applications. Our company has extensive experience in the production of plant-derived natural edible colorants and has obtained quality management systems such as ISO9001 and FSSC22000, as well as FDA certification, HALAL certification, and Kosher certification. The raw materials are carefully sourced from uncontaminated cultivation facilities, ensuring product quality from the raw material stage. As a safe and secure natural colorant, it is widely adopted in the food, beverage, confectionery, and pharmaceutical industries.

Inquire About This Product
basic information
Product Name: Natural Black Tea Derived Brown Color (Black Tea Brown Color) Ingredients: Black Tea (Camellia sinensis) Form: Powder Color Tone: Brown Solubility: Water-soluble (insoluble in fats and ethanol) Characteristics: High coloring power, minimal flavor impact, light and heat stable, purely natural origin Packaging: 1kg, 5kg, 20kg aluminum bags or containers Storage Method: Recommended to store in a dry, light-protected environment Quality Control: Heavy metal and microbiological testing completed, COA available
Price range
Delivery Time
Applications/Examples of results
Food and Beverage Frozen foods, confectionery, dairy products, chocolate Sugar-free foods, ice cream, beverages, jelly, fruit juice products Coloring for canned fish, canned meat, etc. Pharmaceuticals and Cosmetics Coloring agents for sugar-coated tablets and medicinal coatings Applicable to cosmetics as a safe coloring agent derived from natural sources Features and Benefits Purely natural origin, safe and secure Water-soluble with good processability High coloring power with minimal impact on flavor High light and heat stability, easy to preserve and process
Company information
Our company is a global raw material and technology solution provider that offers natural-derived ingredients, including herbal medicines and plant-derived extracts, as well as high value-added functional ingredient formulation technologies. We integrate knowledge of traditional natural materials with modern biotechnology and formulation techniques to cater to a wide range of fields, including pharmaceuticals, health foods, functional foods and beverages, cosmetics, personal care, and animal nutrition. Utilizing advanced technologies such as Cocrystal, Liposomal, microencapsulation, particle technology, pellet technology, and granulation technology, we provide customized solutions to address challenges related to the solubility, absorption, stability, flavor, and processability of functional ingredients. Additionally, we supply a diverse range of natural and functional ingredients, including plant extracts, natural flavors, essential oils, amino acids, and peptides. We have established a consistent global supply system that covers raw material procurement, processing, quality control, and export, allowing us to flexibly respond to development projects from small batches to mass production. Through high-quality raw materials, advanced technologies, and specialized support, we assist customers worldwide in product development and business expansion.