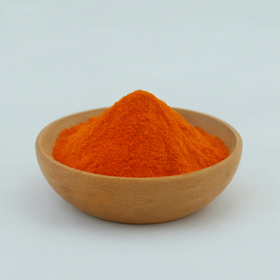
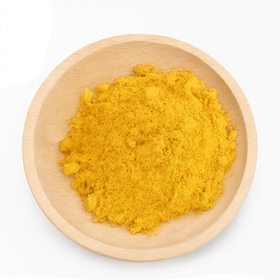
Natural Vitamin E Acetate Microparticle Powder 950 IU Dual-layer Encapsulation and Tablet Pressing
Natural Vitamin E Acetate Microparticles Powder / Natural Vitamin Powder / For Tablet Pressing
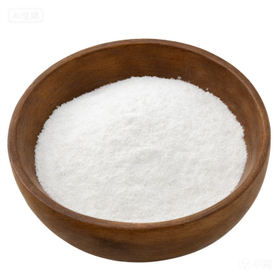
Micronized powder using natural vitamin E acetate. It is designed with a dual-layer encapsulation technology, intended for incorporation into tablet products.
Natural vitamin E acetate microparticle powder is a powdered raw material that uses the acetate form of natural vitamin E. It is designed with a dual-layer encapsulation technology, intended for incorporation into tablet products. Vitamin E acetate is one of the derivatives of vitamin E. This product can be considered when selecting raw materials for products containing natural vitamin E acetate, taking into account not only the content specifications but also the compatibility with powder form and tablet manufacturing processes. In addition to the microparticle powder product form, the design emphasizes dual-layer encapsulation technology and tablet applications. It can be useful for the formulation development of products such as tablet-type health foods and supplements that incorporate vitamin E acetate.
Inquire About This Product
basic information
- Product Name: Natural Vitamin E Acetate Microparticles - English Name: Natural Vitamin E Acetate Microparticles - Specification: 950 IU - Ingredient Name: Vitamin E Acetate - English Ingredient Name: Vitamin E Acetate - Product Form: Microparticle Powder - Processing Technology: Double-layer Encapsulation - Intended Use: For Tablet Compression
Price range
Delivery Time
Applications/Examples of results
This product is a candidate raw material for tablet products containing natural vitamin E acetate. It is available as a microparticle powder using a two-layer encapsulation technology, suitable for formulation development and raw material selection for products involving tablet compression. Expected application areas: - Tablets containing natural vitamin E acetate - Raw materials for supplement tablets - Formulation development for health foods - Raw material selection for products containing vitamin E - Consideration of vitamin raw materials for tablet compression The above are examples of expected applications. Please verify the actual usability and manufacturing suitability according to the formulation design, tablet compression conditions, and quality requirements of the final product.
Company information
Our company is a global raw material and technology solution provider that offers natural-derived ingredients, including herbal medicines and plant-derived extracts, as well as high value-added functional ingredient formulation technologies. We integrate knowledge of traditional natural materials with modern biotechnology and formulation techniques to cater to a wide range of fields, including pharmaceuticals, health foods, functional foods and beverages, cosmetics, personal care, and animal nutrition. Utilizing advanced technologies such as Cocrystal, Liposomal, microencapsulation, particle technology, pellet technology, and granulation technology, we provide customized solutions to address challenges related to the solubility, absorption, stability, flavor, and processability of functional ingredients. Additionally, we supply a diverse range of natural and functional ingredients, including plant extracts, natural flavors, essential oils, amino acids, and peptides. We have established a consistent global supply system that covers raw material procurement, processing, quality control, and export, allowing us to flexibly respond to development projects from small batches to mass production. Through high-quality raw materials, advanced technologies, and specialized support, we assist customers worldwide in product development and business expansion.