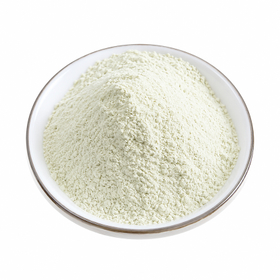
Madder (Rubia) extract powder, natural plant-based functional material.
Rubia Cordifolia Extract Powder - OEM raw material for supplements, cosmetics, and feed additives.
Natural red pigment "munjistin" contained in madder root extract. Ideal for beauty, antioxidant, detox health foods, and dye applications.
Madder (Rubia cordifolia) extract has been a valuable plant material used in traditional Chinese medicine and natural dyes since ancient times. In particular, the natural pigments **Munjistin and Alizarin** found in the root are reported to have functions such as beauty enhancement, antioxidant properties, blood circulation promotion, and anti-inflammatory effects, making them increasingly popular as ingredients in supplements, skincare products, and natural cosmetics in recent years. This product uses high-quality madder cultivated in high-altitude regions such as Inner Mongolia and Yunnan, and the active ingredients are concentrated through water or ethanol extraction and then powdered using spray-drying technology. Despite being a plant-based material, it excels in the coloring power of red pigments and can also be used as a natural coloring agent. This product has obtained various international certifications, including FDA, ISO9001, HACCP, Kosher, Halal, and SC (food production permit), meeting safety standards for food, cosmetics, and feed additives. The powder is uniform and easy to handle, suitable for various processing forms such as beverages, tablets, and topical gels. Small lot production for OEM and ODM applications is also possible. Please consider utilizing this for your product development.

Inquire About This Product
basic information
Product Name: Rubia Cordifolia Extract Powder Extraction Method: Water extraction or ethanol extraction (no solvent residue) Manufacturing Method: Spray-dried after concentration Appearance: Fine powder in reddish-brown to orange-brown color Active Ingredients: Munjistin, Alizarin, etc. Standard Component Content: Total polyphenols ≧5% (reference value) / Pigment components adjustable (OEM available) Moisture: ≦5.0% Particle Size: 80 mesh to 100 mesh Solubility: Soluble in water and ethanol (high dispersibility) Heavy Metal Testing: Lead, arsenic, cadmium, and mercury all below standard limits Microbial Standards: Total Aerobic Bacteria Count: ≦1,000 CFU/g Mold and Yeast: ≦100 CFU/g Coliforms and Salmonella: Negative Packaging: 1kg aluminum bag / 25kg drum (OEM specifications available) Storage Method: Store in a cool, dark place away from high temperature, humidity, and direct sunlight Shelf Life: 24 months from the date of manufacture (unopened)
Price range
Delivery Time
Applications/Examples of results
【Uses in Health Foods】 There is a track record of use in supplements, herbal blends, and powdered beverage products for promoting blood circulation and as beauty ingredients for women. 【Uses in Cosmetics】 Utilizing antioxidant and pigment properties, it is applied in skincare products (whitening and anti-aging) and bath salts. 【Uses as Food Additives】 As a naturally derived red pigment, it meets the demand for natural coloring agents. There is a track record of OEM for plant-based beverages and vegetable soups. 【For Animals and Others】 Can also be used as an immune support ingredient in pet supplements, in natural dye products, and as materials for traditional medicine research.
Company information
Our company is a global raw material and technology solution provider that offers natural-derived ingredients, including herbal medicines and plant-derived extracts, as well as high value-added functional ingredient formulation technologies. We integrate knowledge of traditional natural materials with modern biotechnology and formulation techniques to cater to a wide range of fields, including pharmaceuticals, health foods, functional foods and beverages, cosmetics, personal care, and animal nutrition. Utilizing advanced technologies such as Cocrystal, Liposomal, microencapsulation, particle technology, pellet technology, and granulation technology, we provide customized solutions to address challenges related to the solubility, absorption, stability, flavor, and processability of functional ingredients. Additionally, we supply a diverse range of natural and functional ingredients, including plant extracts, natural flavors, essential oils, amino acids, and peptides. We have established a consistent global supply system that covers raw material procurement, processing, quality control, and export, allowing us to flexibly respond to development projects from small batches to mass production. Through high-quality raw materials, advanced technologies, and specialized support, we assist customers worldwide in product development and business expansion.