iPROS Manufacturing
  • Search for products by classification category

    • Electronic Components and Modules
      Electronic Components and Modules
      62436items
    • Machinery Parts
      Machinery Parts
      75953items
    • Manufacturing and processing machinery
      Manufacturing and processing machinery
      102394items
    • Scientific and Physics Equipment
      Scientific and Physics Equipment
      36710items
    • Materials
      Materials
      38034items
    • Measurement and Analysis
      Measurement and Analysis
      55079items
    • Image Processing
      Image Processing
      15459items
    • Control and Electrical Equipment
      Control and Electrical Equipment
      54791items
    • Tools, consumables, and supplies
      Tools, consumables, and supplies
      65992items
    • Design and production support
      Design and production support
      12663items
    • IT/Network
      IT/Network
      45946items
    • Office
      Office
      14210items
    • Business support services
      Business support services
      27254items
    • Seminars and Skill Development
      Seminars and Skill Development
      6607items
    • Pharmaceutical and food related
      Pharmaceutical and food related
      34760items
    • others
      67829items
  • Search for companies by industry

    • Manufacturing and processing contract
      7351
    • others
      5013
    • Industrial Machinery
      4463
    • Machine elements and parts
      3358
    • Other manufacturing
      2889
    • Trading company/Wholesale
      2708
    • IT/Telecommunications
      2576
    • Industrial Electrical Equipment
      2321
    • Building materials, supplies and fixtures
      1817
    • software
      1675
    • Electronic Components and Semiconductors
      1600
    • Resin/Plastic
      1503
    • Service Industry
      1486
    • Testing, Analysis and Measurement
      1134
    • Ferrous/Non-ferrous metals
      992
    • environment
      699
    • Chemical
      646
    • Automobiles and Transportation Equipment
      599
    • Printing Industry
      514
    • Information and Communications
      474
    • Consumer Electronics
      412
    • Energy
      338
    • Rubber products
      322
    • Food Machinery
      308
    • Optical Instruments
      284
    • robot
      279
    • fiber
      257
    • Paper and pulp
      232
    • Pharmaceuticals and Biotechnology
      174
    • Electricity, Gas and Water Industry
      167
    • Warehousing and transport related industries
      150
    • Glass and clay products
      138
    • Food and Beverage
      135
    • CAD/CAM
      126
    • Medical Devices
      112
    • Educational and Research Institutions
      112
    • retail
      108
    • Ceramics
      98
    • wood
      86
    • Transportation
      85
    • Petroleum and coal products
      67
    • Medical and Welfare
      62
    • Shipbuilding and heavy machinery
      51
    • Aviation & Aerospace
      49
    • equipment
      44
    • Fisheries, Agriculture and Forestry
      42
    • Materials
      38
    • Research and development equipment and devices
      34
    • Public interest/special/independent administrative agency
      32
    • self-employed
      24
    • Government
      23
    • Mining
      17
    • Finance, securities and insurance
      16
    • cosmetics
      16
    • Restaurants and accommodations
      10
    • Individual
      10
    • Police, Fire Department, Self-Defense Forces
      7
    • Raw materials for reagents and chemicals
      5
    • Laboratory Equipment and Consumables
      5
    • Contracted research
      4
  • Special Features
  • Ranking

    • Overall Products Ranking
    • Overall Company Ranking
Search for Products
  • Search for products by classification category

  • Electronic Components and Modules
  • Machinery Parts
  • Manufacturing and processing machinery
  • Scientific and Physics Equipment
  • Materials
  • Measurement and Analysis
  • Image Processing
  • Control and Electrical Equipment
  • Tools, consumables, and supplies
  • Design and production support
  • IT/Network
  • Office
  • Business support services
  • Seminars and Skill Development
  • Pharmaceutical and food related
  • others
Search for Companies
  • Search for companies by industry

  • Manufacturing and processing contract
  • others
  • Industrial Machinery
  • Machine elements and parts
  • Other manufacturing
  • Trading company/Wholesale
  • IT/Telecommunications
  • Industrial Electrical Equipment
  • Building materials, supplies and fixtures
  • software
  • Electronic Components and Semiconductors
  • Resin/Plastic
  • Service Industry
  • Testing, Analysis and Measurement
  • Ferrous/Non-ferrous metals
  • environment
  • Chemical
  • Automobiles and Transportation Equipment
  • Printing Industry
  • Information and Communications
  • Consumer Electronics
  • Energy
  • Rubber products
  • Food Machinery
  • Optical Instruments
  • robot
  • fiber
  • Paper and pulp
  • Pharmaceuticals and Biotechnology
  • Electricity, Gas and Water Industry
  • Warehousing and transport related industries
  • Glass and clay products
  • Food and Beverage
  • CAD/CAM
  • Medical Devices
  • Educational and Research Institutions
  • retail
  • Ceramics
  • wood
  • Transportation
  • Petroleum and coal products
  • Medical and Welfare
  • Shipbuilding and heavy machinery
  • Aviation & Aerospace
  • equipment
  • Fisheries, Agriculture and Forestry
  • Materials
  • Research and development equipment and devices
  • Public interest/special/independent administrative agency
  • self-employed
  • Government
  • Mining
  • Finance, securities and insurance
  • cosmetics
  • Restaurants and accommodations
  • Individual
  • Police, Fire Department, Self-Defense Forces
  • Raw materials for reagents and chemicals
  • Laboratory Equipment and Consumables
  • Contracted research
Special Features
Ranking
  • Overall Products Ranking
  • Overall Company Ranking
  • privacy policy
  • terms of service
  • About Us
  • Careers
  • Advertising
  1. Home
  2. Manufacturing and processing contract
  3. 阪神精工
  4. Product/Service List
Manufacturing and processing contract
  • Added to bookmarks

    Bookmarks list

    Bookmark has been removed

    Bookmarks list

    You can't add any more bookmarks

    By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

    Free membership registration

阪神精工

EstablishmentSeptember 1, 1948
capital1000Ten thousand
number of employees13
addressHyogo/Chuo-ku, Kobe-shi/2-7-7 Wakahama-cho
phone078-251-5595
  • Official site
last updated:Oct 22, 2026
  • Contact this company

    Inquiry Form
  • Company information
  • Products/Services(42)
  • catalog(0)
  • news(0)

阪神精工 Product Lineup

  • category

1~42 item / All 42 items

Displayed results
class="retina-image"

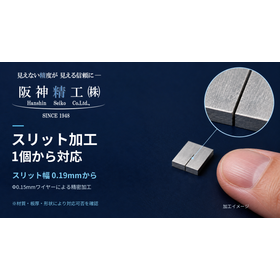
Narrow slit processing | Titanium, carbide, rings, test pieces

Considering processing from a slit width of 0.19mm. Consultations for titanium, carbide, and ring grooves, starting from one test piece.

At Hanshin Seiko Co., Ltd., we utilize wire cut electrical discharge machining and other techniques to accept narrow slit processing from single items, prototypes, and small lots. We consider processing using φ0.15mm wire with slit widths starting from 0.19mm. The feasibility of processing will be individually confirmed based on material, plate thickness, shape, and required precision. You can consult us about narrow cuts in titanium and carbide, groove cuts for pipes and rings, multiple slits for collet chucks, and artificial slits for comparison test pieces used in flaw detection tests. We will confirm not only the groove width but also the cut length, plate thickness, arrangement angle, and remaining wall thickness. We will consider the process while taking into account the opening and deformation after cutting, as well as the holding state during processing. Please also consult us about additional processing for supplied items. For grooves that leave a bottom or artificial notches, we will consider methods suitable for the shape, such as shape-cutting electrical discharge machining.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

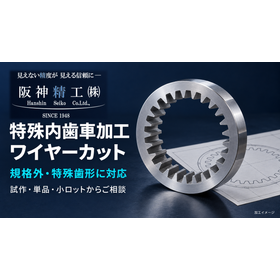
Wire cutting processing of special internal gears | Non-standard tooth profiles and prototypes

For special internal gears that are difficult to prepare dedicated tools for, we will consider individual and prototype non-standard tooth shapes based on drawings and tooth shape data.

At Hanshin Seiko Co., Ltd., we can consult on wire-cut electrical discharge machining for special internal gears and non-standard tooth profiles. For contours that are difficult to handle with standard cutting tools, as well as for single items, prototypes, and small lot products where preparing dedicated tools is burdensome, we will consider machining methods based on drawings and tooth profile data. In addition to basic conditions such as the number of teeth, module, and pressure angle, we will confirm the tooth thickness, tooth groove width, tooth bottom shape, and the positional relationship between the tooth profile center and the reference. Based on the CAD data of the finished contour and the drawings that specify dimensions and tolerances, we will inform you of the feasibility of machining. Please also consult us regarding internal gear machining of hardened materials and high-hardness materials. We will confirm the material, plate thickness, tooth width, required precision, and inspection conditions. When inquiring, please include the purpose of the prototype, assembly confirmation, engagement and operation evaluation, as well as information about the counterpart gear.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

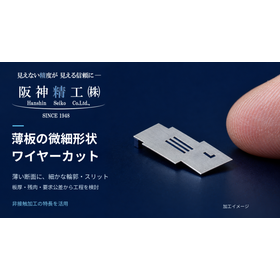
Wire cutting processing of thin plates | Fine contours, irregular holes, slits

For the fine contours, irregular holes, and slits of thin plates. We will check the remaining thickness and holding methods, and consider the processing sequence.

At Hanshin Seiko Co., Ltd., we welcome inquiries regarding wire cut electrical discharge machining for thin plate components with fine contours, irregular holes, and slits. We will consider processing methods tailored to the material, plate thickness, and required precision, including outer shapes with fine steps and notches, square holes, and multiple through slits. Utilizing the characteristics of wire cutting, which does not apply cutting force, we will explore processing methods for thin plates where machining load during cutting is a concern. However, we will also verify the material condition and holding conditions, as there is a possibility of deformation. For multiple slits, the width, length, and spacing are important, as well as the width of the material remaining in between. We will consider the shape during processing, as well as the methods for support and fixation, preparation of starting holes, and processing sequence. Please contact us with drawings that indicate the plate thickness, remaining wall thickness, and tolerances, along with CAD data.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

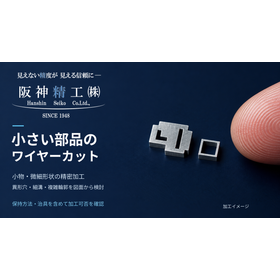
Wire cutting processing of small parts | Irregular holes, fine grooves, contours

For small parts that are difficult to secure. We will consider the holding methods and jigs for irregular holes, fine grooves, and complex contours.

At Hanshin Seiko Co., Ltd., we can discuss wire cut electrical discharge machining for small parts with irregular holes, fine grooves, and complex contours. We will consider processing methods according to the drawings for square holes, through holes with special contours, narrow slits, notches, and asymmetrical outer shapes. Since small parts have limited areas for fixation, we will confirm the reference surfaces, reference holes, machining positions, holding points, and the remaining wall thickness after machining. We will also take into account the state during processing and consider jigs, fixation and support methods, and the order of machining. For fine grooves and small radii, we will check the processing conditions based on wire diameter, discharge gap, plate thickness, and required tolerances. For closed irregular holes, we will also consider the position and preparation method of the starting hole. If you have cases such as "the machining position is close to the edge" or "I want to leave a thin part," please consult us with drawings or CAD data that indicate the dimensions.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Integrated processing of precision small parts | Wire cutting, discharge machining, polishing

From holes, grooves, and contours of small parts to the finishing of reference surfaces. Integrated processing combining wire cutting, discharge machining, and polishing.

At Hanshin Seiko Co., Ltd., we accept the processing of small precision machine parts, mold parts, and jigs. We offer integrated processing tailored to shapes and required precision by combining wire cut electrical discharge machining, shape electrical discharge machining, fine hole electrical discharge machining, machining, and polishing. We consider processing methods for each area, including through holes, irregular holes, outer contour, bottom shapes, fine grooves, small diameter holes, and finishing of plate thickness and reference surfaces. We also examine the positional relationships between holes and outer shapes, grooves, and reference surfaces, and consider methods for transferring processing standards across multiple processes. We plan the processing sequence with consideration for the holding of small parts and the shapes during processing. Please consult us for single items, prototypes, small lot production, and additional processing on supplied items. Please contact us with the overall drawings of the parts, along with material, tolerances, quantities, and desired delivery dates.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Wire cutting processing of slender parts | Contours and through grooves

Processing the contours, through grooves, and notches of elongated parts. We will examine the fixing and supporting methods as well as the processing sequence from the drawings.

At Hanshin Seiko Co., Ltd., you can consult us about wire cut electrical discharge machining for the contours, through grooves, notches, and irregular holes of elongated parts. We will confirm the overall length, width, and thickness of the part, the dimensions of the thin sections that remain after machining, and the positional relationship with reference surfaces and reference holes. We will consider the machining process according to the shape and required precision, including special outer contours and through grooves in the longitudinal direction. As the machining progresses, the parts that can be held and the remaining wall thickness change, so we will also take into account the shape during machining and consider the methods of fixation and support as well as the machining sequence. We will confirm not only the contour dimensions but also the straightness and flatness of the entire part and the specifications of the measurement conditions. Even for additional machining on a specific part, please provide the drawings of the entire part. For special contours, please contact us with the CAD data attached.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Precision machining of thin and small items | Wire cutting and polishing
For those struggling with warping or fixing thin, elongated parts. We will consider the processing steps, including holding methods and processing order.

At Hanshin Seiko Co., Ltd., we can consult on precision machining of thin plates, elongated parts, and frame-shaped components with large openings, focusing on thin and slender items. By combining wire cut electrical discharge machining, polishing, and machining, we will consistently consider the necessary processes from contours, openings, holes, and steps to the finishing of plate thickness and reference surfaces. We will check not only the plate thickness but also the length, width, and remaining wall thickness after processing. We will also take into account the shape during processing and the state after removing fixtures, considering methods of holding, processing standards, and the order of finishing. In addition to dimensional tolerances, please inform us of flatness, parallelism, straightness, surface roughness, and measurement conditions such as support and fixation. For additional processing of supplied items, we will confirm the current shape, warpage, and remaining processing costs to inform you of the feasibility.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Thick material taper wire cutting | Angle-shaped contour processing

Can this thickness and angle be processed? We will examine the tapered holes and inclined contours of thick materials based on the upper and lower shapes and tolerances.

At Hanshin Seiko Co., Ltd., we can discuss taper wire cutting processing for thick parts. We will consider processing methods based on drawings and CAD data for through holes with different dimensions on the top and bottom surfaces, as well as inclined outer contour shapes. The angles that can be processed vary depending on factors such as plate thickness, height, contour shape, and holding conditions. We will not only assess based on the angle but will also check the dimensions of the upper and lower contours, the direction and range of the inclination, and the movement range of the guiding equipment to inform you of the feasibility. In addition to the dimensions of the top and bottom surfaces, we will also confirm the contour in the height direction, dimensional tolerances, angular tolerances, inner corner radii, and surface roughness requirements. We will consider processing conditions and finishing processes. When consulting with us, please provide the upper and lower contour drawings and cross-sectional views, as well as the material, plate thickness, angle, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

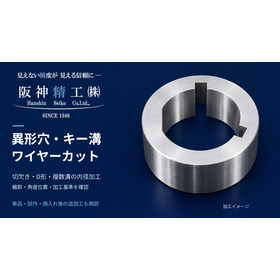
Wire cutting processing of irregular-shaped holes and key grooves | D-shape and notches

A special inner diameter combining key grooves, notches, and D shapes. We also check the angles between the grooves and their positional relationship with the reference.

At Hanshin Seiko Co., Ltd., we offer wire cut electrical discharge machining for through irregular holes, including key grooves, notches, D shapes, and multiple grooves. Please consult us for special single items or prototypes with unique inner diameters that are difficult to process with standard tools, as well as for additional machining on existing holes. We confirm the overall contour of the inner diameter from drawings and CAD data, reflecting the positional relationship with the hole center, outer reference surfaces, mounting holes, and other features into the machining data. For opposing two grooves or multiple evenly spaced grooves, we also check the groove width, depth, and angular position. We will consider adding key grooves or changing the inner diameter contour on parts after hardening, depending on the material, hardness, and required precision. For additional machining on existing holes, we will verify the current shape against the finished contour and check if there is enough material remaining for processing. For stop key grooves and bottomed irregular holes, we can also provide information on alternative methods such as shape cutting electrical discharge machining.
  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

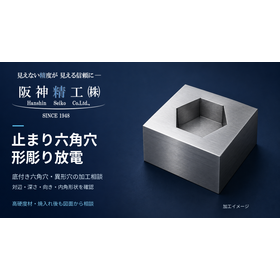
Stop six-sided hole shape engraving discharge machining | High hardness materials, bottomed holes

For hexagonal holes that cannot be penetrated. You can check the dimensions of opposite sides, depth, inner corner radius, and orientation, and we can also discuss additional processing after hardening.

At Hanshin Seiko Co., Ltd., we can discuss the processing of stop hexagonal holes with a remaining bottom, primarily focusing on shape-cutting electrical discharge machining. We consider machining hexagonal holes in shapes where the inner corner curvature interferes with the counterpart parts, as well as additional processing of hexagonal holes in high-hardness materials and parts after hardening. We manufacture electrodes tailored to the hexagonal shape, taking into account the discharge gap and electrode wear. We verify not only the dimensions of the opposite sides but also the required insertion depth, inner corner radius, bottom surface shape, orientation of the hexagon, and the positional relationship with reference surfaces and other holes. Please feel free to consult us about integrated processing that combines wire cutting, machining, and grinding according to the shape. For quotations, please provide a top view and cross-sectional view, along with material, hardness, tolerances, and quantities. For additional processing on existing parts, we will check the current processing state and standards to inform you of the feasibility.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

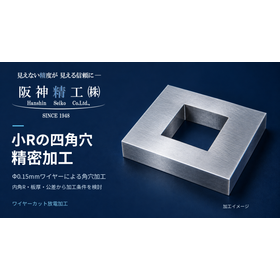
Small R square hole and corner hole processing | Wire cutting

For those who want to reduce the inner corner radius of a square hole. Compatible with a minimum wire diameter of φ0.15mm, and we can also discuss hardened materials.

At Hanshin Seiko Co., Ltd., we accept wire cut electrical discharge machining for square and rectangular holes that require small inner corner radii. Please consult us regarding shapes where the corner rounding becomes significant with end mills, as well as precision corner hole machining for hardened materials. We accommodate wires as small as φ0.15mm. We will review the material, plate thickness, hole width and length, required inner corner radius, and tolerances to consider the machining conditions. We will also check not only the hole dimensions but also the relationship with reference surfaces and other holes, as well as the assembly conditions with counterpart components. For through square holes, we use wire cutting, while for blind holes that require a bottom, we guide you to methods such as shape engraving electrical discharge machining, depending on the shape. Please specify the required R dimensions and allowable ranges on the drawings, and contact us with the quantity and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

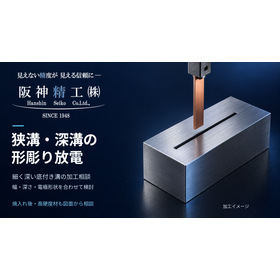
Narrow grooves and fine grooves shape carving electrical discharge machining | Deep grooves and bottomed grooves

We will consider additional processing for the bottomed grooves and high hardness materials from the drawings, where tools cannot fit and the depth cannot be reached.

At Hanshin Seiko Co., Ltd., we accept processing of narrow grooves, fine grooves, and deep grooves, primarily focusing on shape-cutting electrical discharge machining. You can consult us about grooves that are difficult for cutting tools to access, specified grooves with small inner corner radii, and additional processing for high-hardness materials after hardening. We will check not only the groove width but also the depth, length, bottom shape, and end shape. We will consider the production and retention of electrodes, interference with surrounding areas, electrode wear, and discharge of machining chips when determining the processing method. For through grooves, we select wire cutting, while for bottom grooves, we choose methods such as shape-cutting electrical discharge machining or machining, depending on the shape. We can also discuss integrated processing, including grinding, as needed. Please contact us with a cross-sectional diagram of the groove, material and hardness, required tolerances, surface roughness, and quantity. For additional processing on existing parts, we will also check the processing standards and the current work condition.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

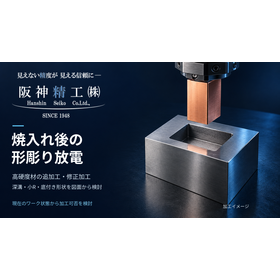
Shape engraving discharge machining after quenching | Additional processing and modification processing

Added deep grooves, small radii, and bottom-contact shapes to the heat-treated parts. Please consult us about shape-engraving electrical discharge machining before remaking.

At Hanshin Seiko Co., Ltd., we accept additional processing and modification of molds and precision parts after heat treatment. We will consider processing methods for high-hardness materials, focusing on shape-cutting electrical discharge machining, including deep grooves, small radii, and bottomed grooves and pockets, which are difficult for cutting tools to reach. We can accommodate design changes after heat treatment, finishing of rough-processed concave shapes, and processing of corners left from cutting. We will check the positional relationship with existing holes, outer shapes, and reference surfaces, as well as the remaining machining allowance and the parts that can be held, and guide you through the processes suited to the current work state. You can also consult us about integrated processing that combines wire cutting, machining, and grinding according to the shape. Please contact us with completed drawings, current processing conditions, and materials indicating additional or modified areas.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

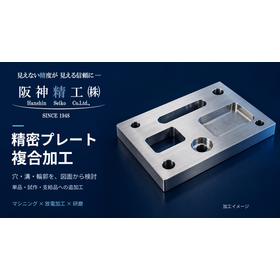
Precision plate processing | Integrated processing of holes, grooves, contours, and polishing

Consistent processing from holes, grooves, and contours to polishing. Supports single-piece production of precision plates, post-hardening processing, and additional work on supplied materials.

At Hanshin Seiko Co., Ltd., we accept orders for the machining of precision plates used in machinery, production equipment, jigs, and molds. We combine machining, wire cut electrical discharge machining, shape electrical discharge machining, fine hole electrical discharge machining, and grinding to provide integrated processing from finishing reference surfaces to holes, grooves, and contours. We will consider processing methods according to shapes such as positioning holes, tapped holes, counterbores, pockets, irregular holes, corner holes, and slits. We will also confirm not only the hole diameter but also the pitch between holes, the positional relationship with the outer shape, and specifications for plate thickness, flatness, and parallelism. We will consider processing standards used in multiple processes and the sequence of operations including heat treatment. In addition to single items, prototypes, and small lot production, please consult us about additional processing for plates after hardening and for supplied items. Based on drawings and CAD data, we will provide guidance on necessary processes and machining feasibility.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

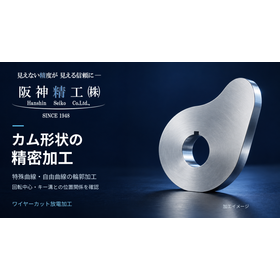
Cam processing | Plate cams and special curves wire cutting

Processing a free curve and asymmetrical shaped plate cam from the drawing. We will also check the relationship between the contour and the positions of the axis hole and key groove.

At Hanshin Seiko Co., Ltd., we offer precision machining of plate cams and special cams used in automatic machines, dedicated machines, and conveying devices. Based on drawings and CAD data that define the finished contours, we consider machining of free curves, asymmetric shapes, and through inner peripheral shapes using wire cut electrical discharge machining. We confirm the positional relationships between the rotation center, shaft holes, key grooves, positioning holes, and cam contours, and reflect this in the machining process. For cam grooves that leave a bottom, we consider suitable methods such as machining or shape-cutting electrical discharge machining based on the shape. Please consult us about integrated machining that combines the necessary processes. We accommodate single-item production for prototype devices, as well as replacement parts and spares for existing equipment. Please contact us with the material, plate thickness, required precision, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

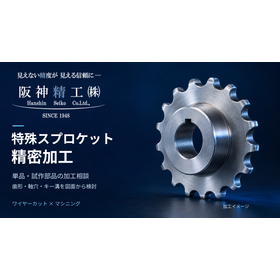
Special Sprocket Processing | Tooth Shape, Shaft Hole, Keyway

For tooth shapes, shaft holes, and keyways that do not fit standard products, please consult us for individual or prototype processing of special sprockets.

At Hanshin Seiko Co., Ltd., we accept consultations for the processing of special sprockets used in conveying devices, dedicated machines, and automatic machines. We will confirm the shapes and positional relationships of tooth profiles, shaft holes, key grooves, and mounting holes, and consider integrated processing that combines wire cut electrical discharge machining and machining. We will reflect the specified angular positions in the drawings during the processing steps, such as aligning the center of the teeth with the center of the key groove. You can consult us about parts that do not fit standard dimensions, thin sprockets, single items for prototype devices, and replacement parts for existing equipment. We will guide you on processing methods tailored to material, plate thickness, quantity, and required precision, whether it involves additional processing of commercial products or manufacturing from raw materials. Please contact us with chain specifications, detailed tooth profile drawings, CAD data, required quantities, and desired delivery dates.
  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

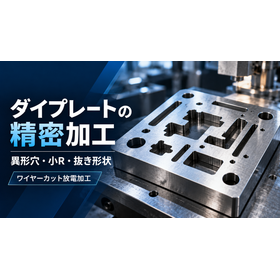
Die plate processing | Irregular holes, small radii, wire cutting

Processing of irregular holes, small R, and cut shapes using wire cutting. Please feel free to consult us for single-piece production of replacement die plates.

At Hanshin Seiko Co., Ltd., we offer precision machining of die plates for press molds. Focusing on wire cut electrical discharge machining, we accommodate processing of irregular holes, inner corners including small radii, narrow slits, and complex cut shapes. We confirm specifications such as clearance with punches, pitch of multiple holes, and positional relationships with reference and locating holes through drawings, and consider processing methods. We also welcome inquiries regarding taper and relief machining in the plate thickness direction, as well as additional machining on die plates after hardening. We can handle wire diameters as small as φ0.15mm. Depending on the shape and finishing conditions, we will consider integrated processing that combines machining, shape cutting electrical discharge machining, and surface grinding. Please feel free to consult us about single-piece production of replacement die plates or remanufacturing based on drawings.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

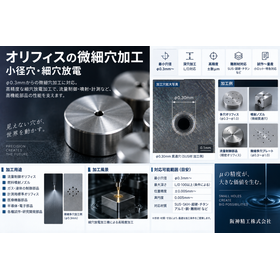
Micro hole processing of orifices | Small diameter hole and fine hole discharge machining

Please consult us about the small diameter hole of the orifice nozzle. We will check the hole diameter and depth, tolerances, and the condition of the inlet and outlet, and consider the processing method using fine hole discharge.

At Hanshin Seiko, we accept inquiries regarding the machining of fine holes and small diameter holes necessary for orifice, nozzle, and flow path components. We have equipment capable of fine hole electrical discharge machining starting from φ0.3mm, and we consider machining small diameter holes that are difficult to process with drills, as well as holes in high-hardness materials such as hardened steel. The feasibility of machining is determined by checking not only the hole diameter but also the combination of material, plate thickness, hole depth, and required precision. In orifices, the hole diameter tolerance, effective length of the hole, and the shape and condition of the inlet and outlet are important. We also confirm the necessary roundness and surface roughness, and consider machining and inspection methods according to the required specifications. We also consider responding to prototypes with different hole diameters, machining multiple holes, and adding holes to supplied parts. If machining of outer shapes, seating surfaces, or reference surfaces is required, please consult us about processes that combine machining, wire cutting, and polishing. Along with the drawings, please provide information on material, hole diameter and tolerance, hole depth, number of holes, quantity, intended use, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

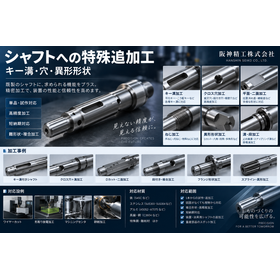
Shaft additional processing | Keyway, D-cut, horizontal hole, irregular shape processing

Additional processing on shafts after lathe machining, hardening, and polishing. We will check the reference positions and angles for key grooves, D-cuts, and cross holes, and consider the holding methods.

At Hanshin Seiko, we accept special additional processing on supplied shafts that have been lathe-turned, heat-treated, and polished. Please consult us about key grooves, D-cuts, two-sided widths, notches, slits, lateral holes, small diameter holes, and irregular holes on end faces. We consider suitable methods for wire cutting, shape electric discharge, fine hole electric discharge, and machining based on material, hardness, and processing shape. We differentiate processing methods according to conditions such as through shapes, bottom shapes, and small diameter holes. For additional processing at multiple locations, we check the axis center, end faces, existing key grooves, and reference holes, taking into account the angular relationship between key grooves and lateral holes, as well as the phase of end face shapes. The polished outer diameter is considered for scratch prevention, and for elongated shafts, we examine the setup based on total length, diameter, processing position, and points that can be held. Please also consult us about additional processing due to design changes or outsourcing only the electric discharge processing steps. Along with a drawing that shows the entire shaft, please inform us of the current processing state, additional processing details, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

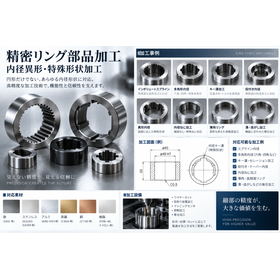
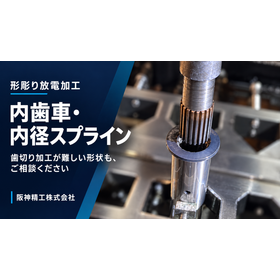
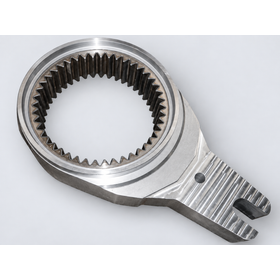
Precision ring component machining | Inner diameter spline and serration

Processing of splines, serrations, and equidistant grooves on the inner diameter of the ring. Consideration is given to the positional relationship with the outer diameter and reference holes, the phase in the circumferential direction, and the deformation of thin-walled sections.

At Hanshin Seiko, we accept orders for the machining of precision ring parts, including inner diameter irregular processing and special shape machining such as splines, serrations, internal teeth, and equidistant grooves. Focusing on wire cut electrical discharge machining, we combine machining, shape-cutting discharge, and polishing as needed, and consider the processing steps according to the drawings. Please consult us for special ring parts in single items, prototypes, or small lots. We confirm not only the inner diameter contour but also the positional relationship with the outer diameter and reference holes, the phase in the circumferential direction, and the angular positions of multiple grooves. For parts with tooth profiles, we create processing data based on specifications such as the number of teeth, pitch, pressure angle, and major and minor diameters. For thin-walled rings, we consider deformation due to fixation and changes in rigidity due to notches, and we examine the minimum wall thickness and holding methods. For parts after quenching, we check the feasibility of processing based on material, hardness, and shape. Along with the drawings and CAD data, please provide information on material, outer diameter, inner diameter, plate thickness, reference position, required tolerances, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

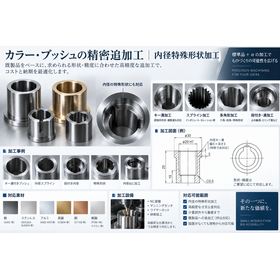
Additional work on color bush | Inner diameter key groove and irregular hole processing

Additional processing of key grooves and irregular holes on turned color bushes. Please consult us for outsourcing wire cutting and electrical discharge machining processes, from single items to small quantities.
At Hanshin Seiko, we accept additional processing for the inner diameters of color bushes manufactured through lathe machining and other methods. We will review the condition of the supplied items and the drawings, and consider manufacturing methods using wire-cut electrical discharge machining or shape-cut electrical discharge machining. You can consult us about inner diameter key grooves, notches, square shapes, multiple grooves in various locations, and asymmetrical irregular holes. If it is possible to pass a wire through a through-hole shape, we will process it using wire cutting while confirming the positional relationship between the existing inner diameter and the additional shape. We also consider responding to single items, prototypes, and small quantities, such as "We can handle lathe machining in-house, but we want to outsource only the special shapes of the inner diameter" or "We don't have enough quantity to prepare a broach." For parts after hardening, we will provide guidance after confirming the material, hardness, and shape. For thin-walled parts, we take into account deformation due to fixation, wall thickness after processing, and the coaxial relationship of inner and outer diameters. Please inform us of the current processing status, quantity, and desired delivery date along with PDF or CAD drawings.
  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Inner diameter spline machining of SCM435 | Die-sinking electrical discharge machining

Case study of spline machining with an inner diameter of 0.8 and 21 teeth. Even small diameter shapes that are difficult to handle with gear cutting equipment will be considered using dedicated electrodes for shape-EDM.

At Hanshin Seiko, we accept consultations for machining the inner diameter splines and internal gear shapes of shafts using shape-cutting electrical discharge machining. The case presented involves machining a tooth profile with a module of 0.8, 21 teeth, and a reference pitch circle diameter of φ16.800mm on the inner diameter of a shaft made of SCM435. We tackled this small-diameter shape, which was difficult to process with the client's gear machining equipment, using a dedicated electrode that matched the tooth profile. We considered the electrode dimensions and machining allowance while taking into account the discharge gap and electrode wear. We aligned the reference of the shaft with the center and axial posture of the electrode, paying attention to the tooth thickness and depth shape. We also considered the discharge of machining chips generated deep within the inner diameter, examining the operation of the machining fluid and electrode. If you have inquiries such as "I can't find a machining source for a small inner diameter" or "I want to add a tooth profile inside the shaft," please send us your drawings. We will confirm the material, heat treatment condition, tooth profile specifications, machining depth, required precision, quantity, and desired delivery date, and provide guidance accordingly.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

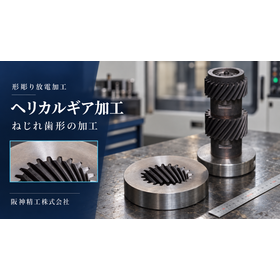
Super hard helical gear shape processing | Copper graphite and shape electric discharge machining

A twisted tooth shape is formed on super hard alloy G7. By using copper graphite electrodes in stages, we perform shape electrical discharge machining that corresponds to rotation and feed.

At Hanshin Seiko, we accept orders for helical gear (hassuba gear) shapes in carbide and complex tooth shapes for electrical discharge machining (EDM). The case presented involves machining a twisted tooth shape in carbide G7. Copper graphite was used for the electrode, and electrodes with side reduction allowances of 0.3mm, 0.15mm, and 0.07mm were selected according to the machining stage. The rotation of the electrode and the axial feed were coordinated along the twisted shape, managing the relationship between machining depth and tooth shape position. During finishing, care was taken to avoid interference with the tooth surface during oscillation and retraction movements, and the process was designed considering electrode wear and the discharge of machining debris. Even after electrode replacement, the reference for the center position and rotation direction is aligned to maintain the positional relationship with the tooth shape from the previous process. Along with drawings and 3D data, please provide information on material, hardness, number of teeth, module, twist angle, machining depth, required precision, surface roughness, quantity, and desired delivery date. We will guide you on the machining methods, including electrode fabrication.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

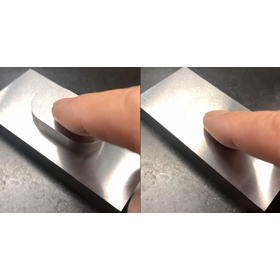
Wire cut processing of composite parts | Achieved gap of approximately 2μm

This is a case of machined fitting parts for delivery, with a clearance of approximately 2μm. We will confirm the required movements and assembly conditions and consider manufacturing based on the drawings.

At Hanshin Seiko, we accept consultations for the production of fitting parts using wire cut electrical discharge machining. The case presented is a block-shaped fitting part with a clearance of approximately 2μm (0.002mm) between the components. We provide photographs of the actual products delivered, showcasing the shapes that fit together and the boundaries between the parts. For fitting parts, it is important to confirm not only the individual shapes and dimensions but also the required movements and assembly conditions when combined. Please provide the material, dimensions, necessary tolerances, intended use, and desired clearance along with the drawings. We will review the specifications and consider the feasibility of processing and manufacturing methods. *The approximately 2μm refers to the gap between the parts in this case. It does not indicate the tolerance of the processing dimensions or the processing accuracy guaranteed for all products.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

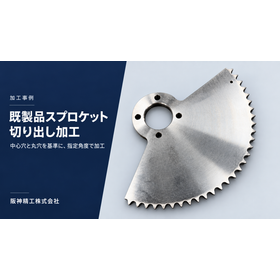
Additional processing of off-the-shelf sprockets | Wire cutting extraction

Leave the necessary dental parts of the ready-made product and cut it out to the specified shape. Determine the position based on the center hole and round hole, and accommodate additional processing with specified angles.

At Hanshin Seiko, we accept consultations for cutting and additional processing using off-the-shelf sprockets. The case presented involves cutting out the necessary tooth section from a standard sprocket and shaping it to the specified form using wire-cut electrical discharge machining. The rotational position was determined based on the center hole and round hole, and the processing was aligned to the specified angle. In additional processing of off-the-shelf products, the positional relationship between existing holes or teeth and the newly processed contour is crucial. The center position is captured from the center hole, and the direction of processing is determined based on its relationship with the round hole. Emphasis is placed on establishing a reference before processing, confirming the relationship between the existing shape and the processing position. For inquiries such as "I want to cut out part of an off-the-shelf product" or "I want to specify an angle relative to the reference hole," please send us the product specifications and processing drawings. We will confirm the material, dimensions, processing range, angle, tolerances, quantity, and desired delivery date to provide guidance.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Processing of internal gears for heat-treated parts | Cast steel, wire cutting

Supports the machining of internal gears on heat-treated cast steel parts. We process specified shapes into the hard tooth areas, taking into account the tooth profile, spacing, and positional relationship with the center.

At Hanshin Seiko, we are considering using wire cut electrical discharge machining for the processing of internal gears and additional machining on hardened parts. The case presented involves the machining of internal gear tooth profiles on the inner circumference of cast steel parts. The tooth areas to be processed have been hardened, and it was required to machine the specified tooth profile on these hard sections. In addition to the material, we confirm the heat treatment condition of the processing area to select the appropriate machining method. We consider not only the individual tooth profiles but also the spacing between the teeth and their positional relationship with the center, setting the machining path according to the requirements of the drawings. We welcome inquiries such as "I want to perform additional machining on hardened parts" or "I want to machine internal gear shapes on hard sections." Please provide us with the drawings along with details on material, heat treatment content, hardness, machining dimensions, tooth profile specifications, required precision, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

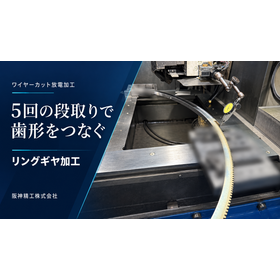
Large diameter ring gear machining | SUS304 - Wire cutting

Machining the tooth profile of a ring gear on a semicircular material with an outer diameter of φ1000mm. Utilizing a unique dedicated jig and five setup steps to accommodate positioning that connects the machining areas.

At Hanshin Seiko, we accept consultations for machining large diameter ring gears and arc-shaped components using wire cut electrical discharge machining. The case presented involves machining a ring gear tooth profile on a half-circle material made of SUS304. The material dimensions are an outer diameter of φ1000mm and an inner diameter of φ950mm, with a total of 656 teeth calculated around the circumference. Since the machining stroke of the machine could not accommodate the entire part, we divided the machining range and processed it in five setups. Using our unique dedicated jigs, we adjusted the position and alignment each time we changed the setup. We ensured that the tooth position, orientation, and the continuity of the arc matched between the previously machined area and the next area. The key point of this case is the setup that considers each tooth profile and the positional relationship of the entire component. For parts that cannot be machined in one setup, we will review the shape, required precision, and holding methods to consider appropriate responses. Please provide the material, outer diameter, inner diameter, plate thickness, tooth profile specifications, required precision, quantity, and desired delivery date along with the drawings.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

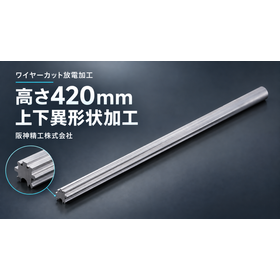
Thick material wire cutting processing | Height 420mm, upper and lower different shapes

A shaft with different shapes at the top and bottom is produced from a material with a height of 420mm. We will consider the program that connects the upper and lower contours and the processing conditions suitable for thick materials.

At Hanshin Seiko, we accept wire cut electrical discharge machining for cutting materials with height and for parts with different cross-sectional shapes at the top and bottom. The example shown involves machining a shaft with different shapes at the top and bottom cut from a material with a height of 420mm. We created the machining program considering not only the upper and lower contours but also the machining surfaces that connect them. For parts with different shapes at the top and bottom, we check the transitions between corners, straight lines, and curves, and consider which positions on the upper and lower sides correspond to each other. To avoid unintended tilting or twisting, we emphasize matching the contours and setting the machining paths. For machining thick parts with a height of 420mm, we adjust the wire tension, discharge conditions, and the supply state of the machining fluid, taking into account the stability of the wire and the condition of the machining surface. If you are looking for machining services for thick parts or parts with different shapes at the top and bottom, please provide the material, dimensions, required precision, quantity, and desired delivery date along with the drawings. We will also assist with short delivery inquiries after checking the machining conditions and operational status.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

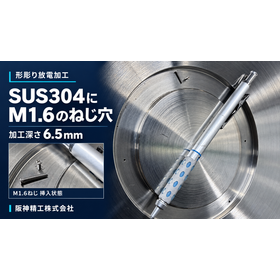
Processing of M1.6 screw holes in SUS304 | Shape cutting discharge and blind holes

A stop screw hole with a depth of 6.5mm and M1.6 size is created in SUS304. The machining chips are repeatedly removed to maintain the discharge state all the way to the bottom of the hole.

At Hanshin Seiko, we accept consultations for machining extremely small screw holes and blind screw holes using shape-cutting electrical discharge machining. The case presented involves machining four blind screw holes of M1.6 with a depth of 6.5mm in a SUS304 component. We processed the screw shape deep into the small holes that do not go through. A key aspect of this case was the removal of machining debris (sludge) that accumulates near the bottom of the hole. We repeatedly removed the sludge as the machining progressed and adjusted the discharge state to continue the machining process. Please consult us about machining small screw holes that are difficult to process with cutting, as well as screw machining for parts that cannot be penetrated. We will also consider the feasibility of screw hole machining in carbide based on material type, screw size, depth, and required precision. Along with the drawings, please provide the material, hardness, screw size and pitch, required screw depth, depth to the bottom of the hole, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

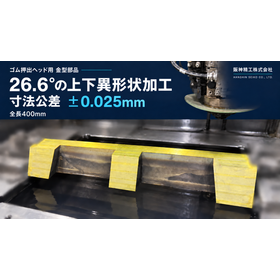
Consistent processing of rubber extrusion molds | Overlapping base

From material to completion, we provide integrated processing in-house. By combining cutting, polishing, wire cutting, and shape electric discharge machining, we manufacture complex rubber extrusion mold components.

At Hanshin Seiko, we offer comprehensive manufacturing of mold components that combines cutting, polishing, wire-cut electrical discharge machining, shape electrical discharge machining, and finishing. The case presented is an "overlapping base" used in rubber extruders such as those for tires. With a total length of 400mm and varying shapes at an angle of 26.6°, we carried out all processes in-house from material to completion, adhering to a dimensional tolerance of ±0.025mm. Considering distortion caused by processing, we designed the process with foresight from the cutting and polishing stages to the subsequent electrical discharge machining. We examined the upper and lower contours and the processing surfaces connecting them, utilizing wire-cut and shape electrical discharge machining as appropriate for the shapes. We welcome inquiries such as "I would like to request parts that require multiple processes together" or "I want to process different shapes on the upper and lower parts to specified tolerances." Please provide us with the drawings along with material, dimensions, required tolerances, quantities, and desired delivery dates.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

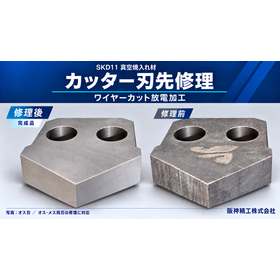
SKD11 cutter blade repair | Wire cutting and grinding processing

Repair of SKD11 vacuum heat-treated male and female blades. Check the condition of the damage and allowable dimensions, and consider reprocessing the blade tips while minimizing the amount of material removed.

At Hanshin Seiko, we accept repairs for cutter blades made of SKD11 vacuum hardening material. The case presented involves the repair of male and female blades used in ceiling panel molding machines. The focus was on removing scratches as much as possible while minimizing the amount of blade edge material removed. We assessed the depth of the scratches and the wear condition to determine whether repairs could be made with an additional removal of approximately 0.05 to 0.1 mm, and decided on the necessary processing amount. The blade edges were finished in multiple stages using wire cut electrical discharge machining, taking into account the required dimensional accuracy and surface roughness. For scratches other than on the blade edges, we combine hand finishing and polishing processes according to the condition. We welcome inquiries such as "I want to remove scratches from the blade edge" or "I want to minimize dimensional changes due to excessive grinding." Please provide us with drawings, photos showing the condition of the scratches, acceptable dimensional changes, quantity, and desired delivery date. *The additional removal amount is based on the conditions considered in this case. The feasibility of repairs and processing amounts will be provided after checking the condition of the actual item and the required specifications.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

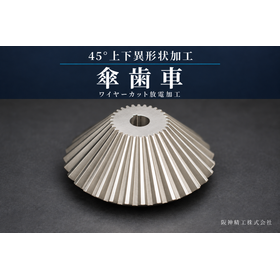
Wire cut processing of bevel gears | 45° upper and lower different shapes

Processing achievements of bevel gears with a 45° upper and lower irregular shape. We tackle the machining of complex tooth profiles through shape verification in CAD and innovative special jigs and processes.

At Hanshin Seiko, we accept consultations for the machining of bevel gears and upper and lower differently shaped parts using wire cut electrical discharge machining. The case presented involves the machining of a bevel gear with a 45° upper and lower different shape. We considered not only the different tooth profiles on the upper and lower sides but also the tooth surfaces connecting them, while examining the shape in CAD and developing the machining program. For complex shapes, in addition to creating the machining path, it is crucial to set up the holding of the product. In this case, we used a special jig and assembled the machining process to fit the product shape. Considering the machining program, holding method, and process as a whole is a key point of our approach. Please feel free to consult us about parts that have "a large inclination and unclear machining methods" or "different shapes on the upper and lower sides that make setup difficult." Along with the drawings and CAD data, please provide the material, dimensions, required precision, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

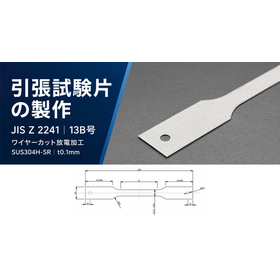
Production of tensile test specimens for thin plates | Plate thickness 0.1mm, wire cutting

Please consult us about thin sheet tensile test specimens with a thickness of 0.1mm. We take into account not only contour accuracy but also warping and scratches after holding, cutting, and removal.

At Hanshin Seiko, we accept the production of tensile test specimens from thin sheet metal based on drawing specifications using wire-cut electrical discharge machining. The article discusses the processing challenges and innovations when producing JIS Z 2241 Type 13B specimens from SUS304H-SR material with a thickness of 0.1mm. For thin sheets, it is important to consider warping and twisting during processing, as well as breakage and scratches during handling, in addition to maintaining stability during processing. We examine support using backing plates and layered cutting according to the condition of the material, while avoiding excessive tightening to ensure stable support until finishing. Attention is also given to the width of the parallel section, the connection with the shoulder radius, and the machining marks at the start and end of the cut. Additional finishing of the machined surface is considered based on applicable standards, drawings, and the requirements of the testing personnel. Please provide the material, heat treatment, thickness, sampling position and direction, quantity, and desired delivery date along with the drawings.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

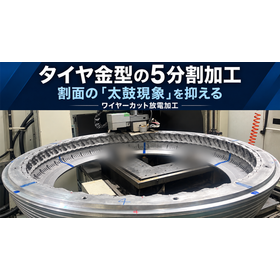
Tire mold split processing | Wire cutting and split surface precision management

Supports 5-part processing of tire molds. We focus on suppressing the drum phenomenon and managing the shape in the thickness direction, pursuing split surface accuracy with assembly in mind.

At Hanshin Seiko, we accept the division processing of tire molds using wire cut electrical discharge machining. The article features the processing of dividing a ring-shaped tire mold into five parts. What we emphasize is not only the accuracy of the division position but also finishing the cut surfaces straight in the thickness direction. We take into account the drum phenomenon, which causes bulges or depressions near the center of the processing surface, and comprehensively consider discharge conditions, processing fluid conditions, wire tension, and feed rate. For large ring-shaped molds, we explore support and holding methods that minimize deformation due to fixation. We also consider the effects of changing rigidity and residual stress as the division progresses, and we organize the setup with an eye on the processing sequence and holding after separation. If you have any concerns about gaps in the cut surfaces or adjustments during assembly, please feel free to consult us. Along with the drawings, please provide information on material, outer diameter, height, weight, number of divisions, cutting costs, required precision of the cut surfaces, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

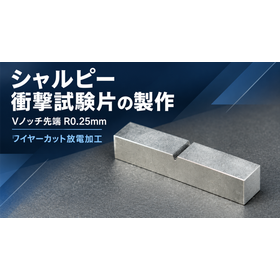
Charpy impact test specimen processing | Wire cutting - V-notch

Please consult us regarding the cutting, shaping, and V-notch processing of Charpy impact test specimens. We will take into consideration specified shapes such as a tip radius of 0.25mm and the processing surfaces.

At Hanshin Seiko, we accept wire-cut electrical discharge machining of Charpy impact test specimens based on provided drawings. We will consider the manufacturing method according to your desired processing range, including cutting from the material, contour machining, and V-notch processing. For specified shapes such as a V-notch with a tip radius of 0.25mm, we take into account the notch depth, angle, tip radius, and the contour connecting the slope to the tip radius. We combine wire diameter, discharge gap correction, feed, tension, and processing fluid conditions to perform finishing cuts according to your requirements. We confirm the sampling position of the test specimen, material direction, and the surface where the notch will be created, processing while inheriting the identification information of the supplied material. If necessary, we will also consider preparing reference surfaces through cutting or grinding. Along with the drawings, please provide information on material, heat treatment condition, applicable standards and versions, surface roughness, inspection requirements, quantity, and desired delivery date. We will check the scope of processing, finishing, and inspection and provide guidance accordingly.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

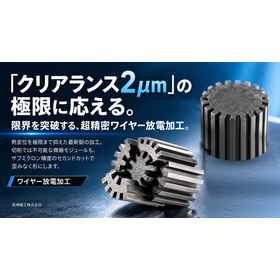
Precision Gears and Fine Tooth Profile Processing | Wire Cut Electric Discharge Machining

A case study of precision gear machining aimed at a clearance of 2μm. We pursue fine tooth shapes through multiple cuts, temperature management, and condition adjustments at the root of the teeth.

At Hanshin Seiko, we accept consultations for precision gears, fine tooth profiles, and complex contour shapes processed by wire cut electrical discharge machining. The case presented involves the processing of gear shapes with a target clearance of 2μm (0.002mm). We approached this considering the finish of the tooth surface, corner radii at the root, temperature variations, and wire vibrations. After rough machining, we performed multiple finishing cuts, gradually adjusting the machining cost and discharge energy. We aimed to reduce temperature differences through temperature management of the machining fluid and pre-soaking of the workpiece, while adjusting the movement speed and discharge conditions at the root. Please consult us for parts requiring narrow clearances or tooth profiles with small corner radii. Along with your drawings, please provide material, plate thickness, required tolerances, specified clearance locations, quantity, and desired delivery date. *Note: 2μm is the target clearance for this case and does not indicate achieved measured values or a uniform guaranteed accuracy.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

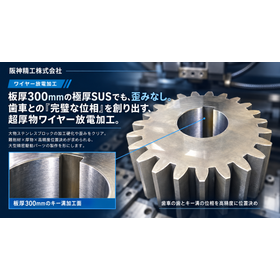
Processing of thick key grooves in SUS304 | Wire cut electrical discharge machining

Processing results for a large SUS304 gear with a thickness of 300mm. Care is taken with the shape accuracy in the thickness direction and the alignment of the key groove to the outer peripheral tooth profile.

At Hanshin Seiko, we offer wire cut electrical discharge machining for thick stainless steel parts such as SUS304. The case presented involves the machining of key grooves for a large gear made of SUS304 with a plate thickness of 300mm. In addition to the shape accuracy in the thickness direction, "phase management" became important to align the angle and positional relationship of the key groove with respect to the outer circumference of the tooth profile. In thick material processing, we consider the deflection of the wire and the discharge of machining chips, and we examine wire tension, processing fluid pressure, and discharge conditions. We separate the roles of rough machining and finishing, and assemble the process while paying attention not only to the entrance and exit but also to the shape of the intermediate sections. We also take into account positioning based on the tooth profile and any changes in posture during fixation. Please consult us regarding key groove machining for thick parts and additional machining where the positional relationship with the tooth profile is specified. Along with the drawings, please provide the material, dimensions, weight, required tolerances, machining position, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

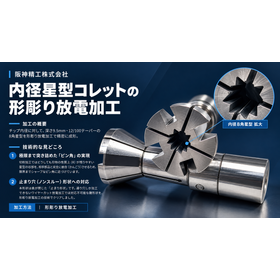
Inner diameter processing of an 8-point star-shaped collet | Shape engraving discharge and blind holes

Example of inner diameter processing of a tapered octagonal star shape. Consideration is given to the discharge of chips from the stopped shape and electrode wear, while pursuing sharp corners in the valley area.

At Hanshin Seiko, we accept consultations for inner diameter processing of special collets using shape-engraving electrical discharge machining, as well as for complex shapes such as star-shaped and polygonal designs. The case presented involves inner diameter processing of an octagonal star-shaped collet with a tapered stop shape of 12/100 and a depth of 9.5mm. Sharp pin angles were required in the valley portions of the star shape. In addition to electrode design that considers discharge gap and electrode wear, we examine the relationship between electrode reduction allowance and swing amount. We pursue processing conditions that maintain the taper shape while preventing corners from becoming excessively rounded. For stop shapes, we also consider the flow of processing fluid to ensure that chips do not accumulate at the bottom or in the valleys. Please consult us regarding inner diameter shapes that are difficult for cutting tools to access, as well as special shapes with bottoms. Along with your drawings, please provide material, processing depth, required tolerances, allowable corner R, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

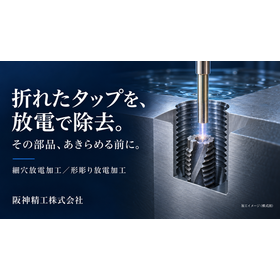
Broken tap removal and deburring processing | Fine hole discharge and shape engraving discharge

Before giving up on parts due to tap breakage. We will consider a method for removing broken tools that minimizes damage to the threads using small hole discharge and shape cutting discharge.

At Hanshin Seiko, we offer the removal of broken taps and reworking through fine hole electrical discharge machining and shape engraving electrical discharge machining. If you have a situation where "the tap broke deep inside the screw hole," "it's too hard to drill," or "the extractor has broken off," please consult us for assistance with molds, jigs, and precision parts that are in the processing stage. We will check the size, material, position, and depth of the broken tool, and consider the size and shape of the electrode, positioning, and discharge conditions. We will select methods that minimize damage to the surrounding threads and base material, such as removing the center of the tap and extracting the remaining fragments. After removal, we will check the condition of the screw hole and consult on the necessity of additional processing or repairs if needed. Please provide us with a photo of the broken area, the tap size, the material of the base, the work dimensions, and your desired delivery date. *Please note that processing may not be possible depending on the state of the breakage. We do not guarantee that the threads will remain undamaged or that the part can be reused after removal.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

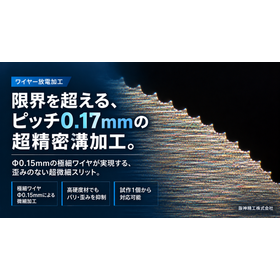
Micro groove and micro slit processing | Wire cut electrical discharge machining

Case study of continuous groove machining with φ0.15mm wire and a pitch of 0.17mm. We will consider discharge conditions, fluid pressure, and machining sequence taking into account the thin-walled shape.

At Hanshin Seiko, we accept consultations for machining fine grooves, fine slits, and narrow pitch shapes using wire cut electrical discharge machining. The case presented involves continuous fine groove machining with a pitch of 0.17mm between the centers of grooves, using a φ0.15mm wire electrode. In the case of fine continuous grooves, it is necessary to consider not only the formation of the grooves but also the thin sections left between them. We take into account the wire diameter and discharge gap to determine the machining width, as well as the discharge energy, machining cost, fluid pressure, and machining sequence. We will confirm the material, plate thickness, groove width, pitch, required tolerances, and necessary remaining thickness dimensions, and provide guidance on the appropriate machining methods based on the shape. Please feel free to consult us about fine parts with comb-like or multi-groove shapes that you may be struggling to process. Based in Kobe City, Hyogo Prefecture, we respond to inquiries from across the country. Please provide us with your drawings, quantities, and desired delivery dates.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

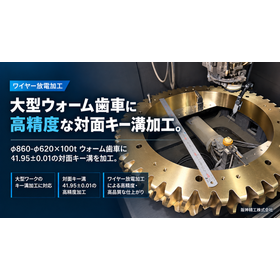
Keyway machining for large gears | Wire cutting and face keyway

Machining record for a worm gear with an outer diameter of φ860mm. We will machine precision keyways, taking into consideration the alignment of the rotation direction and the protection of existing surfaces.

At Hanshin Seiko, we process key grooves for large gears and worm gears using wire cut electrical discharge machining. We welcome inquiries about additional processing for parts with internal face key grooves or those requiring positional alignment in the direction of rotation. The example featured is the processing of face key grooves on a large worm gear with an outer diameter of φ860mm, an inner diameter of φ620mm, and a thickness of 100mm. In addition to the specified dimension of 41.95±0.01mm, we undertook processing that required alignment in the direction of rotation. We pay attention to fine rotational adjustments of large workpieces, position verification after fixing, and prevention of scratches on tooth surfaces and finishing surfaces. We manage the dimensions of the grooves and the processing positions separately, emphasizing setups that protect the existing shapes. We accommodate single items, prototypes, small lots, and additional processing for supplied materials. Based in Kobe, we accept processing inquiries from across the country. Please provide us with the drawings along with material, weight, condition of the workpiece, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration

Hastelloy X/XR shape engraving electrical discharge machining | Chamfering and corner relief machining

Supports the preparation and corner escape processing of Hastelloy. We accept complex shapes and additional processing on supplied materials using dedicated electrodes for shape engraving electrical discharge machining.

Hanshin Seiko offers shape machining and electrical discharge machining for Hastelloy X and Hastelloy XR. Using dedicated copper electrodes, we process beveled shapes and corner reliefs or notches on the inner corners. Please consult us for areas where cutting tools are difficult to access or for additional machining on existing parts. We will confirm the material, shape, required tolerances, and machining depth, and consider the electrode shape, discharge gap, positioning references, and protection of existing surfaces in our machining methods. We accommodate single items, prototypes, and small lots. Based in Kobe City, Hyogo Prefecture, we accept requests from across the country through material and parts delivery. Please provide us with the drawings, material, work condition, quantity, and desired delivery date.

  • Electric discharge machine

Added to bookmarks

Bookmarks list

Bookmark has been removed

Bookmarks list

You can't add any more bookmarks

By registering as a member, you can increase the number of bookmarks you can save and organize them with labels.

Free membership registration
Prev 1 Next
  • 脱炭素×高出力×軽量 天吊式・人感センサ付 速暖式工場用暖房機
  • 全3回・無料ウェビナー 規制情報の収集・管理に課題はありませんか? 毎月100件以上施行される新しい規制に対応するためのソリューションをご紹介
    • Contact this company

      Inquiry Form

    Products

    • Search for Products

    Company

    • Search for Companies

    Special Features

    • Special Features

    Ranking

    • Overall Products Ranking
    • Overall Company Ranking

    support

    • site map
    IPROS
    • privacy policy Regarding external transmission of information
    • terms of service
    • About Us
    • Careers
    • Advertising
    IPROS Services
    • >IPROS GMS | Search site for the manufacturing industry
    • >IPROS | Search site for the B2B industry
    COPYRIGHT © 2001-2026 IPROS CORPORATION ALL RIGHTS RESERVED.
    Please note that the English text on this page is automatically translated and may contain inaccuracies.