
List of Manufacturing and processing machinery products
- classification:Manufacturing and processing machinery
226~270 item / All 102854 items


Reduce the workload from handling heavy objects! Here are five case studies that solved customer challenges! We are also accepting free consultations and tests tailored to your work!

- Other conveying machines


No more need to lift heavy one-gallon cans! Enjoy comfortable liquid transfer in the central kitchen.
- Other Pumps
Decision to exhibit at the 1st Chubu Food Industry Creation Exhibition '26!
We will be exhibiting at the "1st Chubu Food Industry Creation Exhibition '26" to be held at Port Messe Nagoya from November 4 (Wednesday) to November 6 (Friday), 2026. As a new addition to our lineup, we will showcase the "Cordless Sanitary Handy Pump," which is a product we started selling in April last year, alongside our "Compact Sanitary Handy Pump Model MHS." - Cordless! Portable anywhere! Easy to use! Simple cleaning! It is compatible with standard 18L cans and BIB (Bag-in-Box) and features a structure that allows for easy disassembly and cleaning. We would like to invite you to visit us at this opportunity. - Venue: Port Messe Nagoya - Our exhibition booth: Hall 1 "C-66"
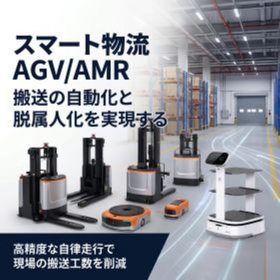

We integrate high-precision autonomous transport robots and business AI to achieve the automation and depersonalization of transport processes within factories, as well as the visualization of equipme...
- Other industrial robots
- Transport and handling robots
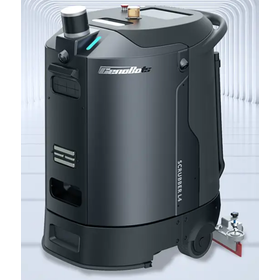

Intelligent navigation, close cleaning near edges, and a maintenance-friendly design provide consistent cleaning performance even in crowded environments.
- Industrial Vacuum Cleaners
- Other industrial robots
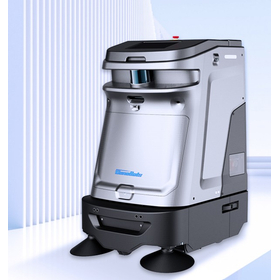
The world's first full-fledged spot cleaning robot.
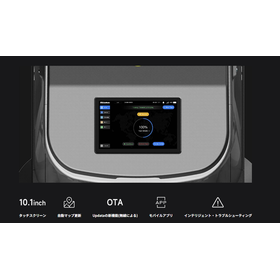
- Other industrial robots
- Industrial Vacuum Cleaners

Without stopping, it turns. The Magic Roller Q improves the efficiency of the parts supply line.
- Sorting machine

A upgraded model that improves the stability and maintainability of vehicle assembly.
- Other conveying machines
- Conveyor

Support for improving efficiency on set with the Electric Elevating Inverter Light Skip (LSG).
- Other conveying machines
- Food Conveyor Equipment

Toho University Trust's power base in network management projects with strict pace constraints.
- Other conveying machines

Smoothly change the direction of the automotive parts assembly line at a right angle on the same plane.
- Conveyor

Automatic diving lift for weight pallets and racks! Supports 24-hour continuous operation with 30-minute rapid charging and 8 hours of operation.
- Other industrial robots
- Transport and handling robots
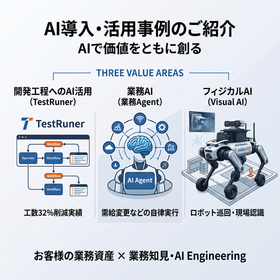
From sudden demand change emails to inventory inquiries, impact analysis, and core system reflection. Autonomizing veteran-dependent tasks.
- Other industrial robots
- Transport and handling robots
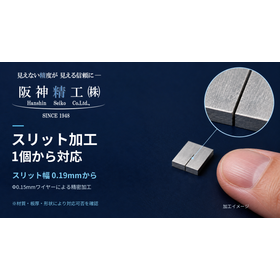

Considering processing from a slit width of 0.19mm. Consultations for titanium, carbide, ring grooves, and test pieces starting from one unit.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
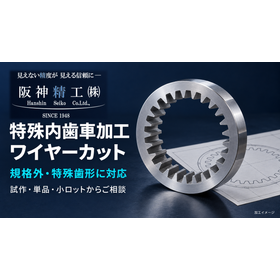
For special internal gears that are difficult to prepare dedicated tools for, we will consider individual and prototype non-standard tooth shapes based on drawings and tooth shape data.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
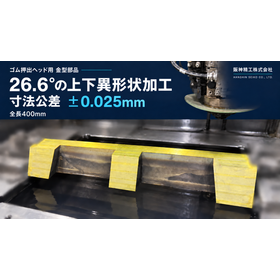
From material to completion, we provide integrated processing in-house. By combining cutting, polishing, wire cutting, and shape electric discharge machining, we manufacture complex rubber extrusion m...
- Electric discharge machine
- Contract manufacturing
- Processing Contract
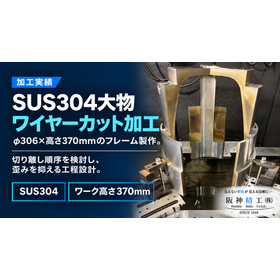
Consultation on the separation of cylindrical and cup shapes. Considering residual stress and changes in rigidity, we will examine the processing sequence, centering, and holding methods.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
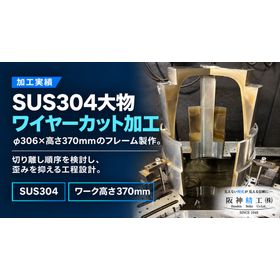
Processing example of SUS304 large frame | φ306 × height 370mm - ingenuity in cutting sequence
We would like to introduce a machining case where a frame for a buoy retrieval device was manufactured from a cup-shaped workpiece made of SUS304. Three large sections were cut away from the side wall of the workpiece with an outer diameter of φ306mm and a height of 370mm, forming an opening and an arch-shaped contour. The height of 370mm refers to the outer dimensions of the workpiece and should be distinguished from the actual thickness of the material being cut. The official article discusses the cutting sequence considering the release of residual stress and changes in rigidity, centering using a dial gauge, and methods of holding, along with photos taken before and after machining. For inquiries regarding the machining of large and hollow shapes, please provide the drawings and photos before machining, as well as the material, overall dimensions, wall thickness, machining range, required tolerances, quantity, and desired delivery date. For more details, please refer to the official article linked in the related links.
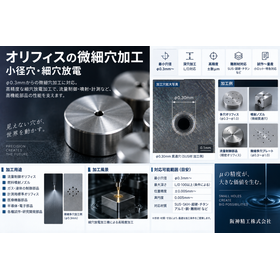
Please consult us about the small diameter hole of the orifice nozzle. We will check the hole diameter and depth, tolerances, and the condition of the inlet and outlet, and consider the processing met...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
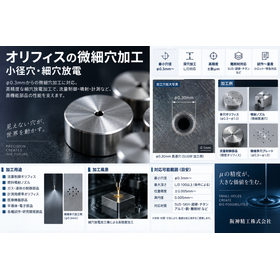
Processing of fine holes, deep holes, and hardened materials | Fine hole electrical discharge machining, nationwide support from single item prototypes.
Introducing the fine hole discharge machining by Hanshin Seiko Co., Ltd. We can handle hole machining for small diameter holes and deep holes that are difficult to drill, using a thin pipe-shaped electrode, as well as for high-hardness materials such as hardened steel and cemented carbide. We accommodate start holes for wire cutting, small diameter holes for orifices and nozzles, and additional machining of holes after heat treatment. We have equipment capable of processing fine holes starting from φ0.3mm. The hole diameter range according to equipment specifications is φ0.3 to 3.0mm for the MEMH-8 model and φ0.3 to 6.0mm for the JEM50FD. The actual processable hole diameter, depth, and tolerance vary depending on the material and shape, so we will provide guidance after reviewing the drawings or CAD data. Our service page introduces fine hole machining for orifices, small diameter and deep hole machining, and methods for removing broken taps. Based in Kobe City, we accept requests from across the country for single items, prototypes, and small lots. We can also facilitate the delivery of parts from distant locations through shipping companies. Please consult us for integrated processing from wire cutting and shape engraving discharge machining to machining and polishing.
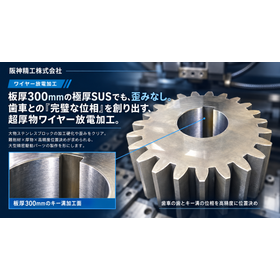
Processing results for a large SUS304 gear with a thickness of 300mm. Care is taken with the shape accuracy in the thickness direction and the alignment of the key groove to the outer peripheral tooth...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
Wire cutting and electrical discharge machining from Okayama and Kurashiki | Information on key grooves and additional processing for thick parts.
Hanshin Seiko Co., Ltd. has published information regarding wire cutting and electrical discharge machining consultations for companies in Okayama Prefecture, including Okayama and Kurashiki. The processing base is located in Kobe City, Hyogo Prefecture. Consultations can be conducted without visiting the site through meetings based on drawing data and the transfer of parts via a transportation company. We will consider processing methods for thick gears with inner diameter key grooves, irregular hole processing based on existing holes and tooth shapes, and additional slits after hardening. In addition to shape-cutting electrical discharge and fine hole electrical discharge, please consult us for integrated processing that includes machining and polishing. The page features a case study of key groove processing for large gears made of SUS304 with a thickness of 300mm. It includes points to confirm in thick material processing, such as shape in the thickness direction, alignment with tooth shapes, and methods for securing the entire part. For large and heavy items, we will also confirm packaging, transportation, and unloading conditions along with the feasibility of processing. Please contact us with drawings, material, quantity, required precision, desired arrival date, and the overall dimensions and weight of the parts.
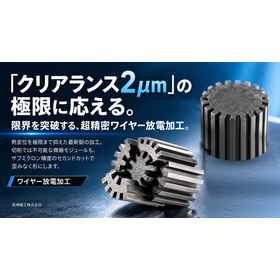
A case study of precision gear machining aimed at a clearance of 2μm. We pursue fine tooth shapes through multiple cuts, temperature management, and condition adjustments at the root of the teeth.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
Is the precision the same for everyone with high-precision machining? An explanation of wire cutting and skilled craftsmanship.
Hanshin Seiko Co., Ltd. has published a technical article titled "With high-precision machining machines, will the accuracy be the same regardless of who performs the machining? | Wire cutting and skilled techniques." The accuracy of a product involves not only the performance of the equipment but also the confirmation of the machining location, reference surfaces, and fixed positions, the selection of machining conditions, as well as measurement and correction. The article introduces necessary judgments in the field using examples of parts with thick materials, stepped shapes, and holes in the machining path. It explains the approach of measuring the upper, middle, and lower parts of thick materials and reviewing wire tension and machining speed based on the results. It also discusses the advancements in automatic control and the role of humans, as well as skill inheritance utilizing condition records and past achievements. This can also be viewed as a checklist when selecting a machining company. If you are considering machining thick materials, complex shapes, or tight tolerances, please consult us with drawings that specify the material, dimensions, machining locations, and tolerances.
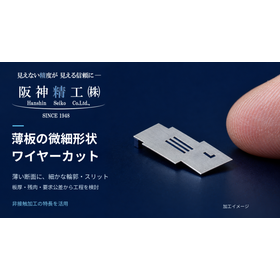
For the fine contours, irregular holes, and slits of thin plates. We will check the remaining thickness and holding methods, and consider the processing sequence.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
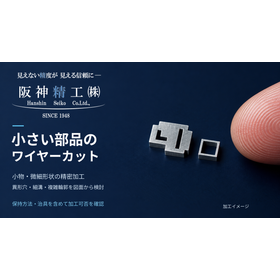
For small parts that are difficult to secure. We will consider the holding methods and jigs for irregular holes, fine grooves, and complex contours.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
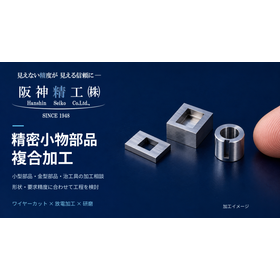
From holes, grooves, and contours of small parts to the finishing of reference surfaces. Integrated processing combining wire cutting, discharge machining, and polishing.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
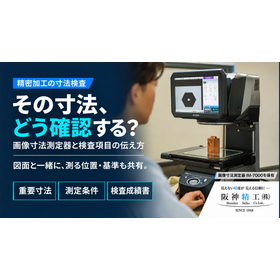
Explanation of dimension verification in precision machining | How to communicate measurement positions, standards, and inspection records.
This article introduces the confirmation of dimensions for precision machined parts and explains the inspection items to be communicated at the time of ordering. Hanshin Seiko possesses the image dimension measuring device IM-7000. The article organizes the differences in display units and measurement accuracy, as well as the differences in contours and internal shapes that can be confirmed through images, summarizing the key points for aligning the understanding of inspection conditions. At the time of quoting, please inform us of the important dimensions, tolerances, measurement positions, references, methods, inspection quantities, and whether an inspection report is required along with the recorded items. We will confirm the details of our response, submission format, costs, and delivery times in advance. This explanation is intended to clarify the distinction between the number of display digits of the measuring device and the machining accuracy or inspection guarantees for all items, and to consider methods that align with the drawings. For more details, please refer to the official article linked in the related links.
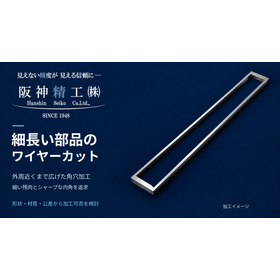
Processing the contours, through grooves, and notches of elongated parts. We will examine the fixing and supporting methods as well as the processing sequence from the drawings.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
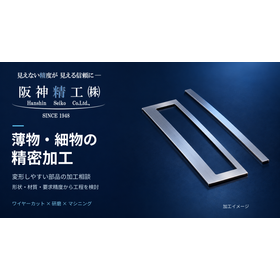
For those struggling with warping or fixing thin, elongated parts. We will consider the processing steps, including holding methods and processing order.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
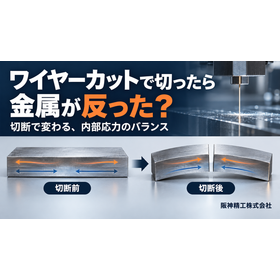
Why does metal warp during wire cutting? An explanation of the processing steps considering residual stress and deformation.
Hanshin Seiko Co., Ltd. has published a technical article titled "Did the Metal Warp When Cut by Wire EDM? Unexpected Deformations in Precision Machining." Even with wire cutting, which does not apply cutting forces from blades, the balance of residual stress within the material changes due to the cutting process, potentially leading to warping, distortion, and the opening and closing of slits. The article shares our experience of rapid movement of the material during the splitting of large rings. It explains key points for considering processes with anticipated deformations, such as the material's processing history, cutting sequence, fixation methods, retention after separation, and measurements during processing. Additionally, it discusses the differentiation of deformations caused by fixation and the thermal effects of discharge, as well as accuracy checks in both fixed and removed states. If you are facing issues with machining thin plates, elongated parts, or rings, or dealing with warping after cutting, please consult us with your drawings, material and heat treatment history, required precision, and any documentation of past deformation situations.
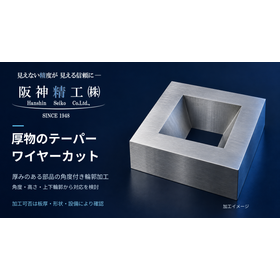
Can this thickness and angle be processed? We will examine the tapered holes and inclined contours of thick materials based on the upper and lower shapes and tolerances.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
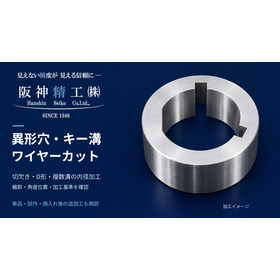
A special inner diameter combining key grooves, notches, and D shapes. We also check the angles between the grooves and their positional relationship with the reference.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
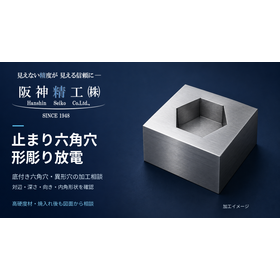
For hexagonal holes that cannot be penetrated. You can check the dimensions of opposite sides, depth, inner corner radius, and orientation, and we can also discuss additional processing after hardenin...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
For those who want to reduce the inner corner radius of a square hole. Compatible with a minimum wire diameter of φ0.15mm, and we can also discuss hardened materials.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
Explanation of wire cutting corner R | Considerations for wire diameter, groove width, and corner relief.
We would like to introduce an article that explains the relationship between the inner corner radius of wire cutting, wire diameter, and processing groove width. The inner corners will retain a curvature based on the wire radius and discharge gap. The article organizes guidelines for the R based on finishing conditions, differences between the cutting width in one pass and the final groove width, and key points to consider for corner relief and chamfering to avoid interference with counterpart parts. At Hanshin Seiko, we utilize wires of φ0.30, φ0.25, φ0.20, and φ0.15 mm according to the processing requirements. The finished R and groove width cannot be guaranteed by wire diameter alone. Please consult us with details such as material, plate thickness, required R and tolerance range, groove width, tolerances, counterpart parts, quantity, and desired delivery date. We will also confirm the possibility of changes to the drawings. For more details, please refer to the official article.
We will consider additional processing for the bottomed grooves and high hardness materials from the drawings, where tools cannot fit and the depth cannot be reached.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
Added deep grooves, small radii, and bottom-contact shapes to the heat-treated parts. Please consult us about shape-engraving electrical discharge machining before remaking.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
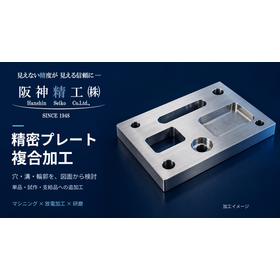
Consistent processing from holes, grooves, and contours to polishing. Supports single-piece production of precision plates, post-hardening processing, and additional work on supplied materials.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
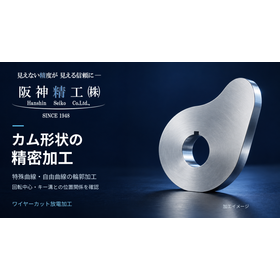
Processing a free curve and asymmetrical shaped plate cam from the drawing. We will also check the relationship between the contour and the positions of the axis hole and key groove.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
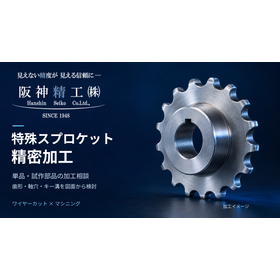
For tooth shapes, shaft holes, and keyways that do not fit standard products, please consult us for individual or prototype processing of special sprockets.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
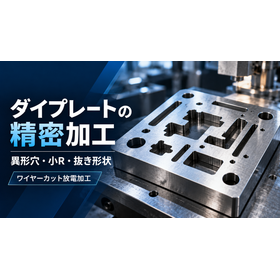
Processing of irregular holes, small R, and cut shapes using wire cutting. Please feel free to consult us for single-piece production of replacement die plates.
- Electric discharge machine
- Processing Contract
- Contract manufacturing
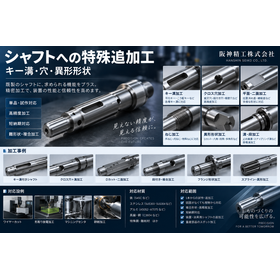
Additional processing on shafts after lathe machining, hardening, and polishing. We will check the reference positions and angles for key grooves, D-cuts, and cross holes, and consider the holding met...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
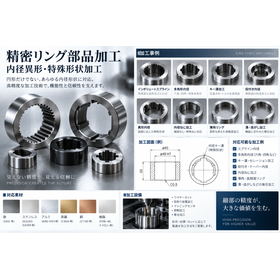
Processing of splines, serrations, and equidistant grooves on the inner diameter of the ring. Consideration is given to the positional relationship with the outer diameter and reference holes, the pha...
- Electric discharge machine
- Contract manufacturing
- Processing Contract
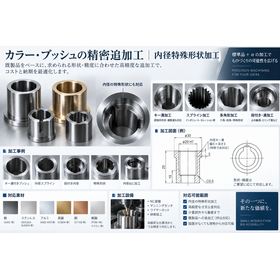
Additional processing of key grooves and irregular holes on turned color bushes. Please consult us for outsourcing wire cutting and electrical discharge machining processes, from single items to small...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
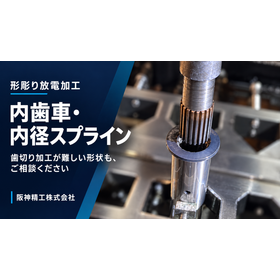
Case study of spline machining with an inner diameter of 0.8 and 21 teeth. Even small diameter shapes that are difficult to handle with gear cutting equipment will be considered using dedicated electr...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
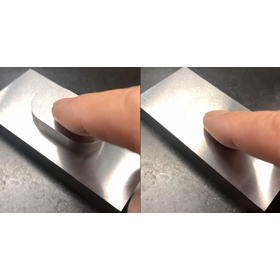
This is a case of machined fitting parts for delivery, with a clearance of approximately 2μm. We will confirm the required movements and assembly conditions and consider manufacturing based on the dra...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
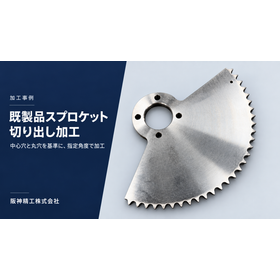
Leave the necessary dental parts of the ready-made product and cut it out to the specified shape. Determine the position based on the center hole and round hole, and accommodate additional processing ...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
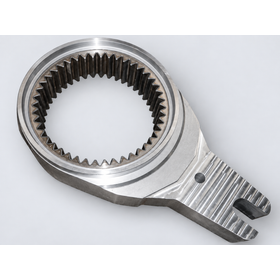
Supports the machining of internal gears on heat-treated cast steel parts. We process specified shapes into the hard tooth areas, taking into account the tooth profile, spacing, and positional relatio...
- Electric discharge machine
- Contract manufacturing
- Processing Contract
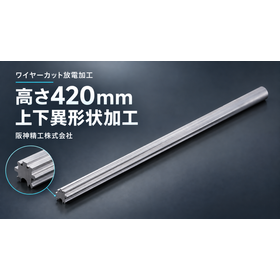
A shaft with different shapes at the top and bottom is produced from a material with a height of 420mm. We will consider the program that connects the upper and lower contours and the processing condi...
- Electric discharge machine
- Processing Contract
- Contract manufacturing
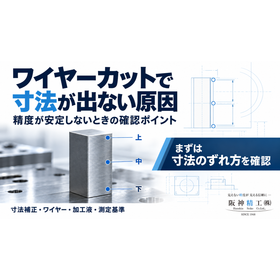
What are the causes of dimensional issues in wire cutting? An explanation of the differences in thickness, die shape, and key points to check.
Hanshin Seiko Co., Ltd. has published a technical article titled "Causes of Dimension Issues in Wire Cutting | Checkpoints When Precision is Unstable." Issues such as "not achieving the desired dimensions," "dimensions differing between the top and bottom," and "only the intermediate section not matching the shape" highlight the importance of distinguishing whether there is a consistent dimensional deviation overall or if the shape of the machined surface is changing in the thickness direction. The article introduces factors to check, including correction amounts, wire deflection and vibration, machining fluids, material deformation, and temperature. It also explains our response examples, where we checked the top, middle, and bottom of thick materials and adjusted the machining feed rate and wire tension based on the measurement results. Please consider the approach of understanding the nature of the deviations and reviewing machining conditions rather than judging solely by correction values or the number of finishing passes. For inquiries regarding machining of thick materials with strict tolerances, please contact us with the drawings, material, thickness, and required precision. If you have already machined parts, please also provide the actual measurements and remaining machining allowances.
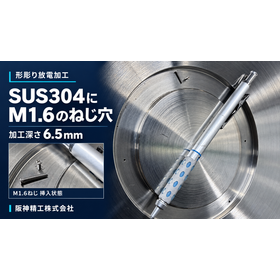
A stop screw hole with a depth of 6.5mm and M1.6 size is created in SUS304. The machining chips are repeatedly removed to maintain the discharge state all the way to the bottom of the hole.
- Electric discharge machine
- Processing Contract
- Contract manufacturing